In the fast-paced world of product manufacturing, efficiency and precision in the final packaging stage are non-negotiable. Shuttle packaging machines have emerged as a cornerstone technology for businesses aiming to scale their output while maintaining impeccable quality and consistency. This guide delves into the core aspects of shuttle packaging systems, exploring their various types, significant benefits, and providing a structured framework for selecting the ideal machine for your specific operational needs.
Understanding Shuttle Packaging Machines
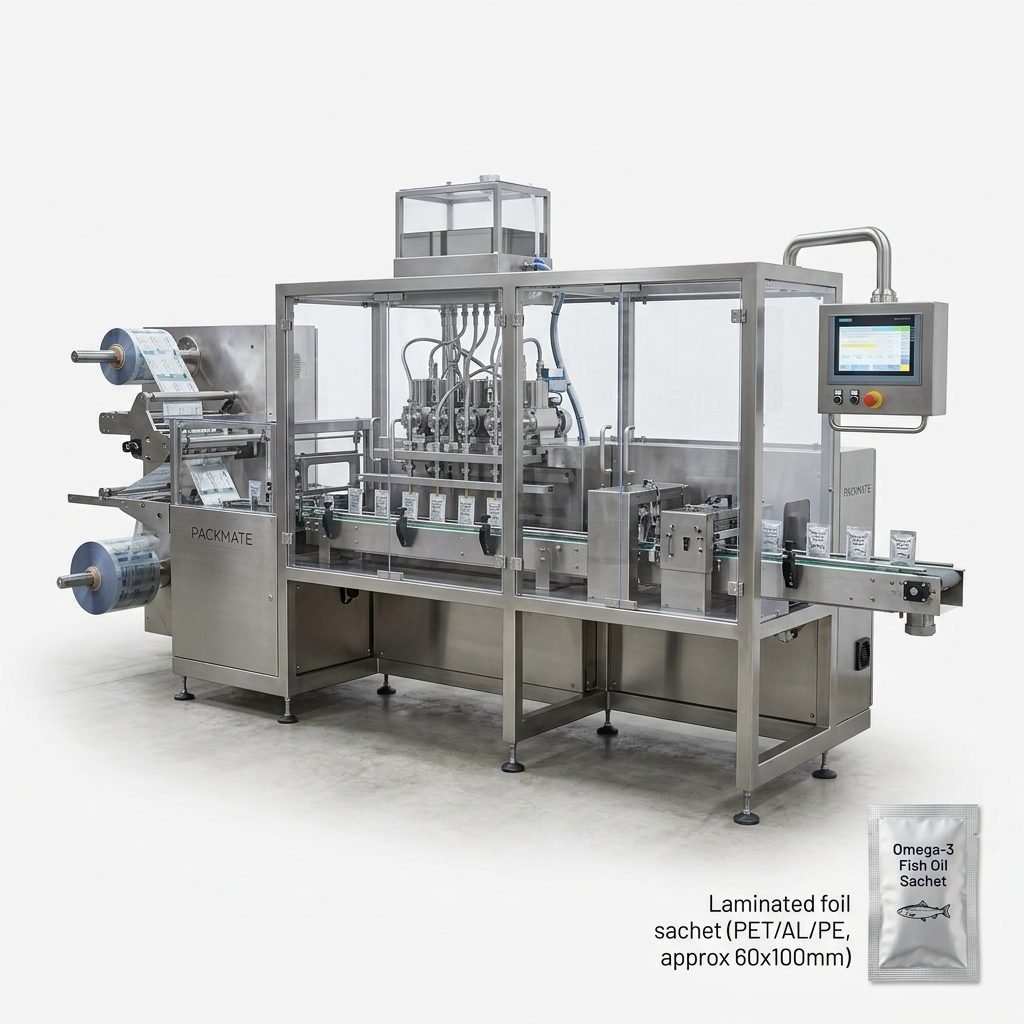
A shuttle packaging machine is a type of form-fill-seal (FFS) equipment characterized by its reciprocating, or “shuttling,” motion. Unlike rotary systems, a shuttle machine typically features one or more forming tubes that move back and forth. This motion allows for precise film feeding, forming, sealing, and cutting, making it exceptionally versatile for producing a wide range of pouch styles. The core principle involves pulling packaging film over a forming shoulder, shaping it into a tube around the filling nozzle, creating vertical seals, filling the product, and then creating the horizontal top seal before cutting the finished pouch loose.
This method is particularly renowned for its accuracy in registration control, which is crucial for printed films, and its gentle handling of products, making it suitable for everything from fine powders and granules to delicate snacks and viscous liquids.
Primary Types of Shuttle Packaging Machines
The market offers several configurations of shuttle machines, each designed to optimize different production goals. Understanding these types is the first step in making an informed purchase.
Single-Tube Shuttle Machines
As the foundational model, a single-tube shuttle machine is ideal for lower to medium production volumes, pilot projects, or products requiring frequent changeovers. Its simplicity offers ease of operation and maintenance. It’s perfectly suited for businesses entering automated packaging or those with a diverse but lower-volume product portfolio.
Dual-Tube (or Multi-Tube) Shuttle Machines
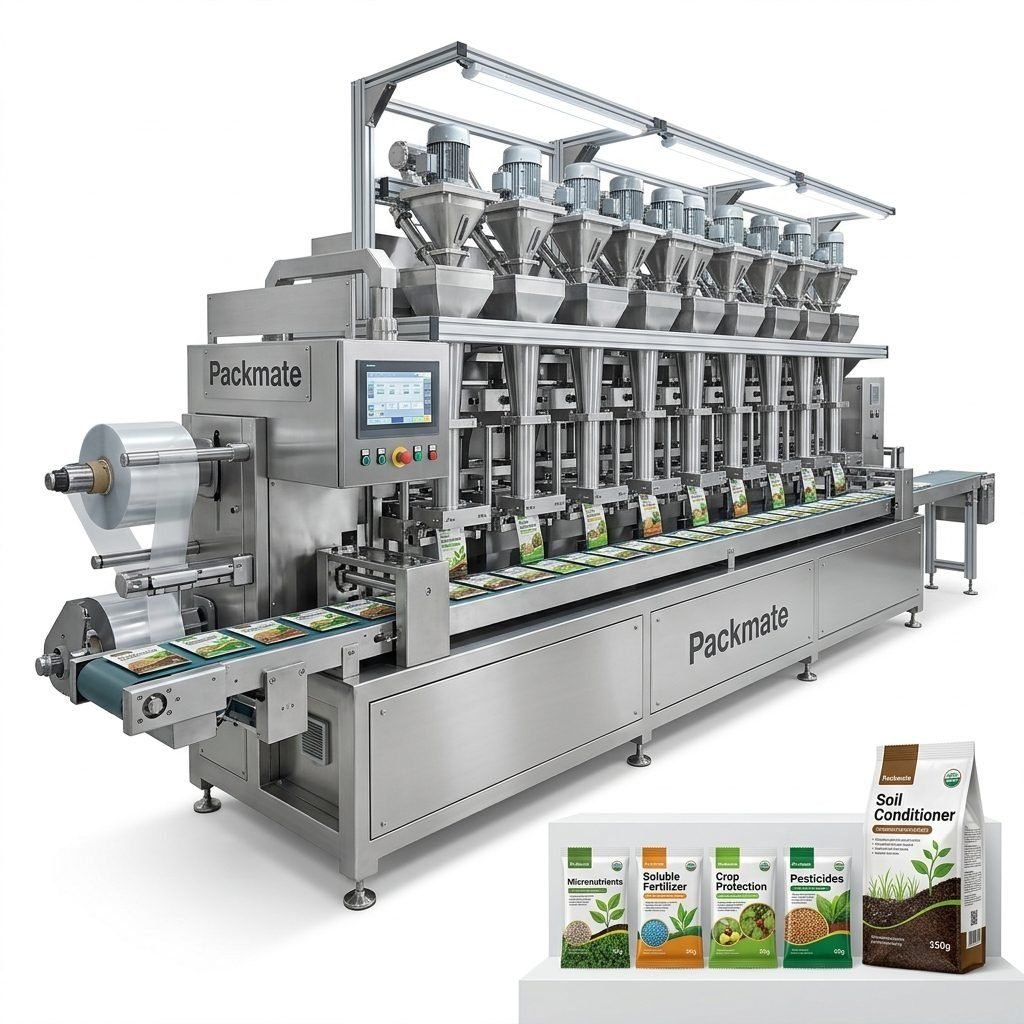
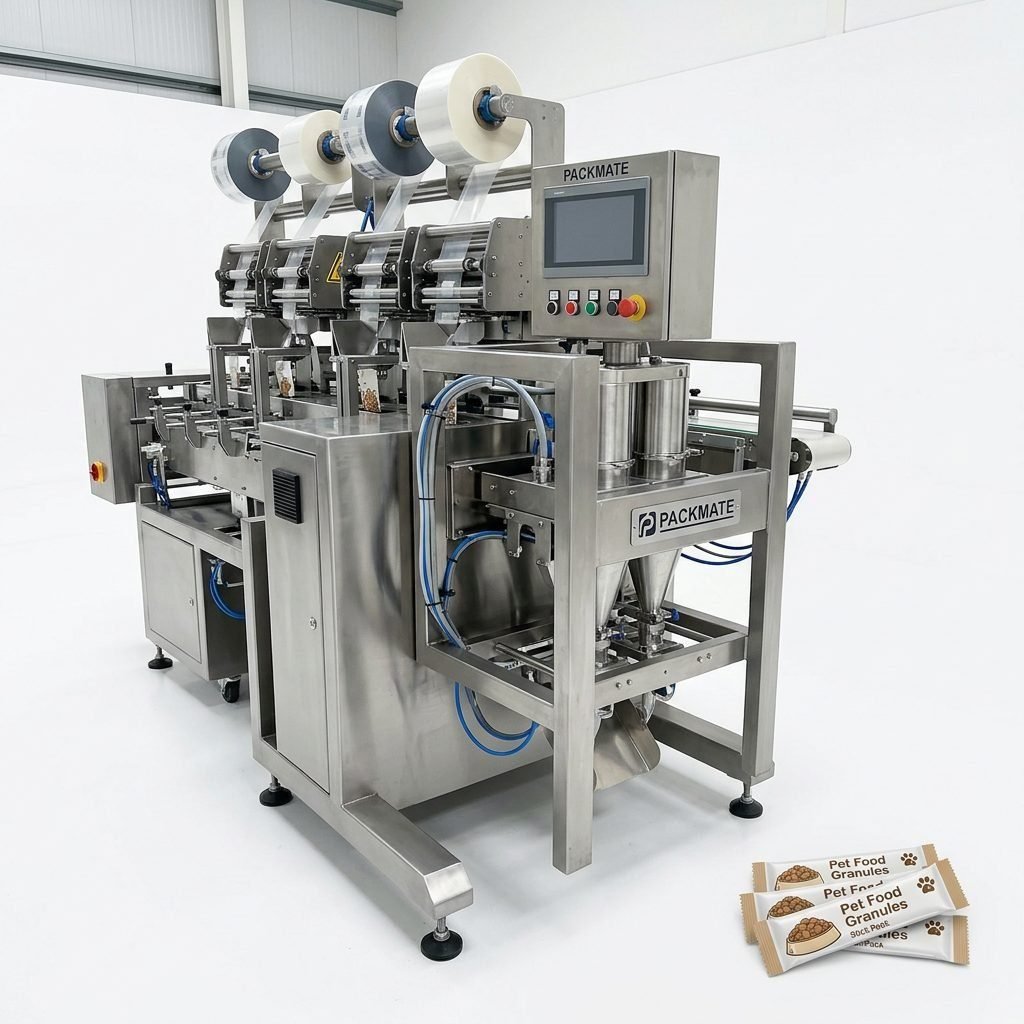
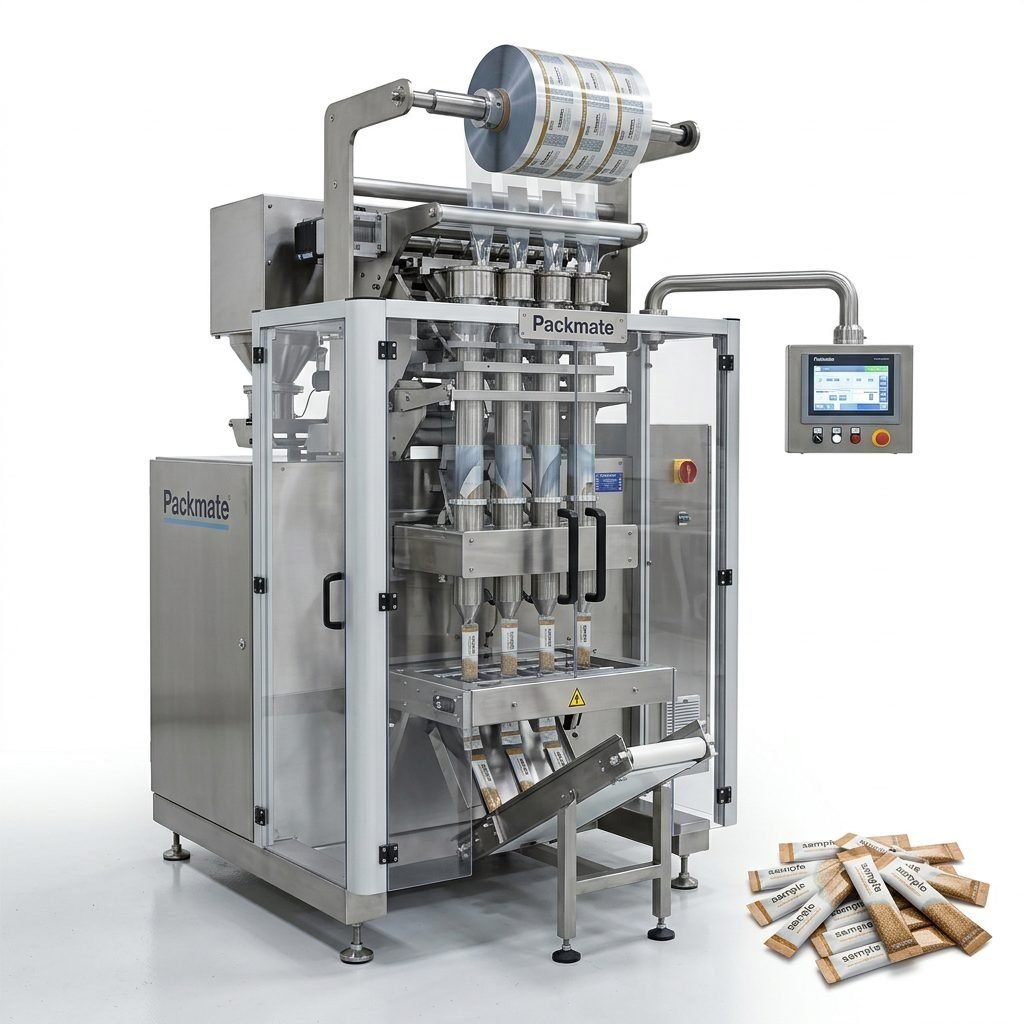
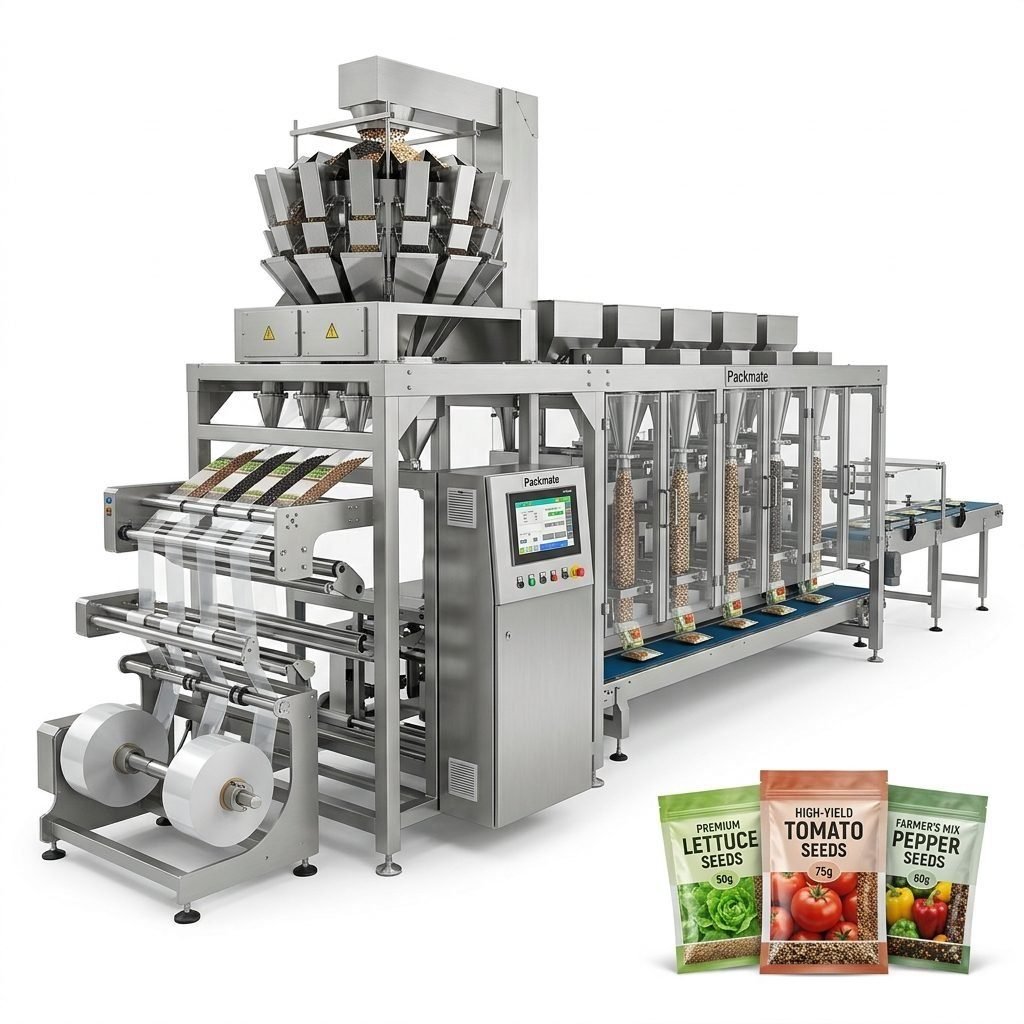
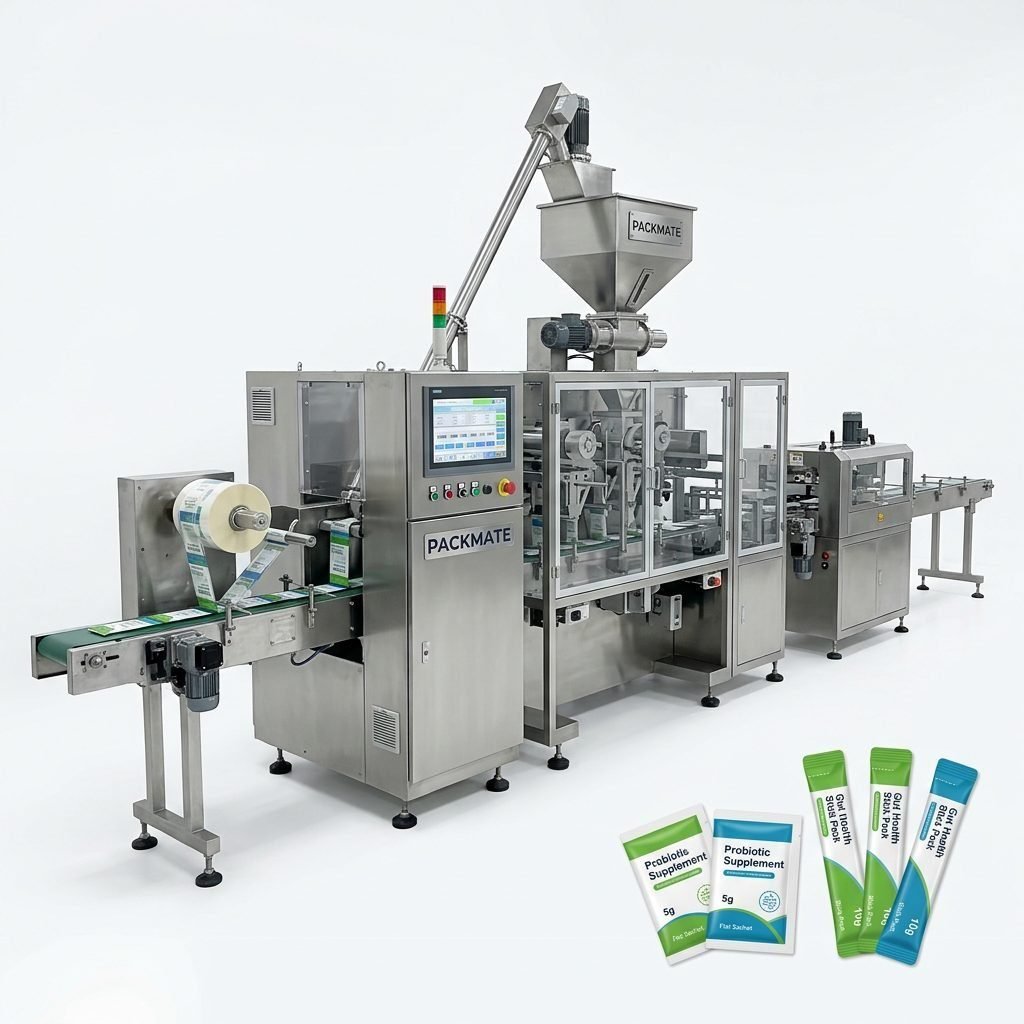
For operations demanding higher output, dual or multi-tube shuttle machines double or multiply the production capacity within a similar footprint. Each tube operates independently, allowing for simultaneous packaging of the same or even different products. This type significantly boosts efficiency and is a common choice for high-volume sachet and stick pack production in industries like food and pharmaceuticals.
Integrated Weighing & Shuttle Systems
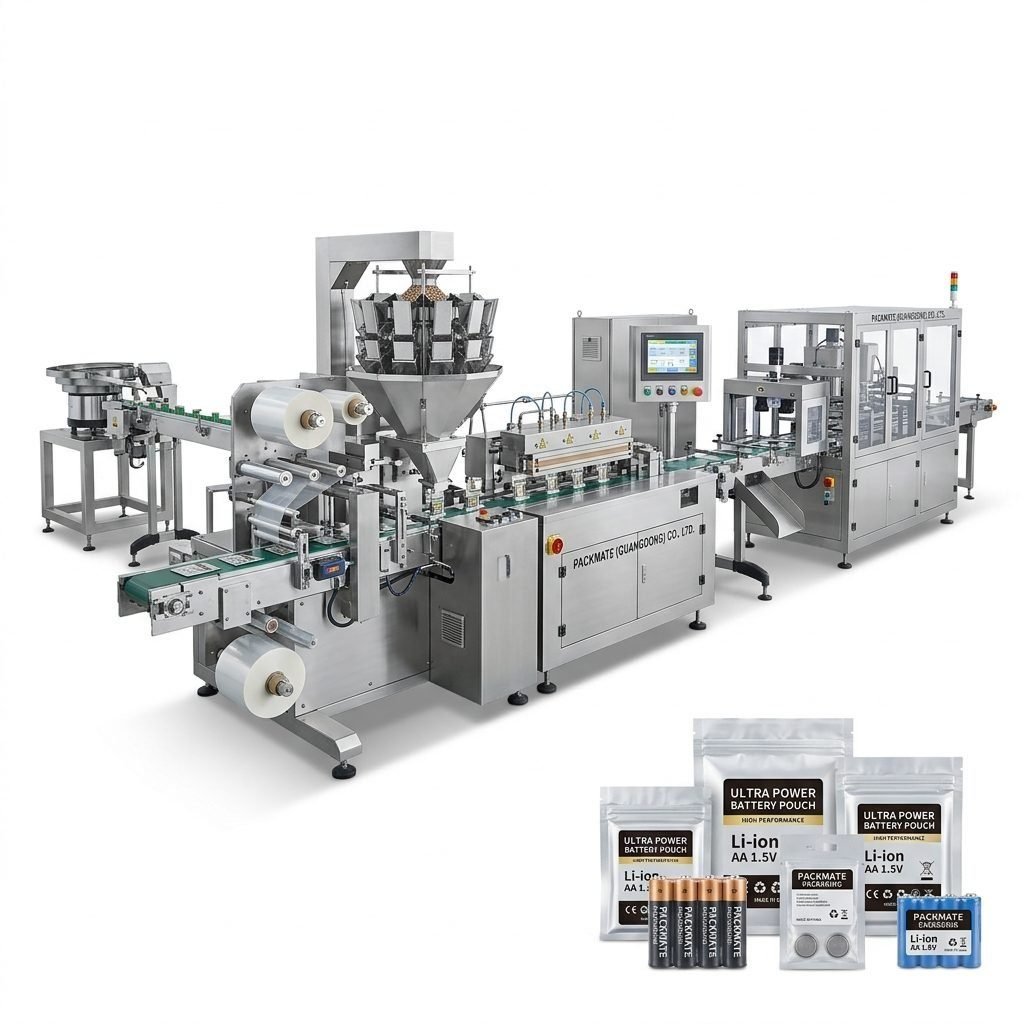
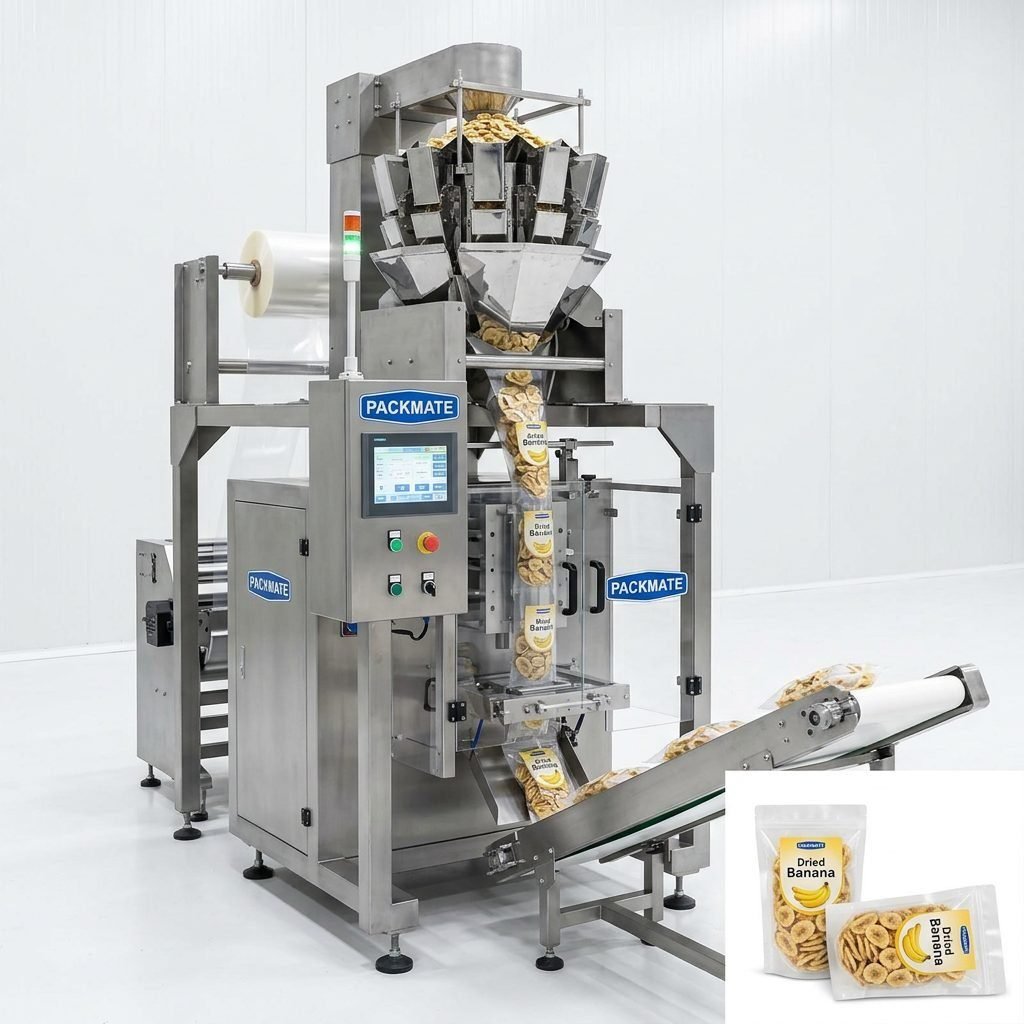
This advanced configuration combines a precision multi-head weigher or auger filler directly with the shuttle packaging machine. It creates a seamless, automated line for products sold by weight, such as snacks, nuts, or hardware components. The integration minimizes transfer points, reduces product giveaway, and ensures remarkable speed and weight accuracy, forming a complete weighing and packaging system.
Key Benefits of Implementing Shuttle Technology
Investing in a shuttle packaging system translates to tangible operational advantages that directly impact the bottom line and product quality.
Enhanced Packaging Versatility: Shuttle machines can handle a vast array of materials, including laminated films, aluminum foil, and biodegradable composites. They can produce various pouch styles such as pillow bags, gusseted bags, and stand-up pouches with high integrity seals.
Superior Seal Quality and Product Protection: The controlled, linear motion allows for consistent pressure and dwell time during the sealing process. This results in strong, hermetic seals that are critical for extending shelf life, preserving freshness, and preventing contamination, especially vital for food and pharmaceutical filling lines.
Precision and Reduced Waste: Excellent film registration control ensures graphics are perfectly aligned on every pouch, enhancing brand presentation. Accurate cutting and sealing minimize film waste, while precise filling systems reduce product giveaway, optimizing material usage.
Gentle Product Handling: The smooth shuttling action is less aggressive than some high-speed rotary motions, making these machines ideal for fragile products like chips, crackers, or instant noodles that must remain intact.
Operational Flexibility: Modern shuttle machines are designed for quick changeovers. With features like recipe memory storage and tool-less adjustments, switching between different pouch sizes or products can be achieved in minutes, maximizing uptime and supporting small-batch production runs.
How to Choose the Right Shuttle Packaging Machine
Selecting the optimal machine requires a careful analysis of your current and future needs. Here is a step-by-step framework to guide your decision.
1. Define Your Product and Packaging Specifications
Start with the basics. What are you packaging? Define the product’s physical state (powder, granule, liquid, solid), its characteristics (abrasive, oily, fragile), and its required dosage or weight. Next, detail the packaging: pouch dimensions, film type and thickness, required seal type (e.g., 4-side seal, back seal), and any special features like zippers or spouts.
2. Evaluate Required Production Capacity
Calculate your required output in pouches per minute (PPM). Consider your current daily volume and projected growth for the next 3-5 years. A single-tube machine may suffice for 40-120 PPM, while multi-tube systems can reach 300+ PPM. Always allow for a 15-20% capacity buffer to accommodate peak demand.
3. Assess Integration and Automation Needs
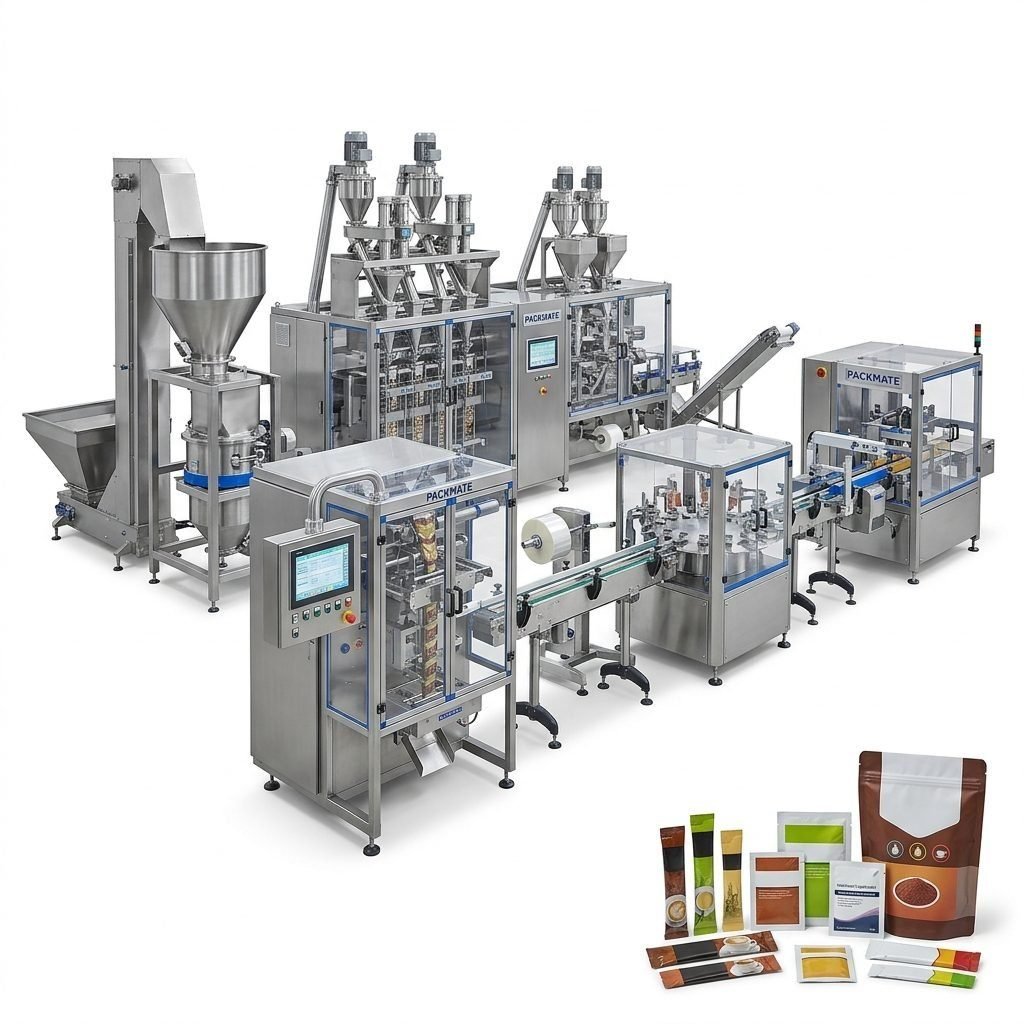
Determine if you need a standalone machine or a fully integrated line. Will it need to connect to upstream equipment like mixers or downstream systems like cartoners? Consider the level of automation required—semi-automatic feeding vs. fully automated systems with robotic palletizing. For complex lines, partnering with a provider like Packmate Machinery, which offers turnkey solutions, can streamline integration and ensure compatibility.
4. Prioritize Ease of Use and Maintenance
Look for user-friendly interfaces (often touchscreen HMIs) with intuitive controls and multi-language support. Machines designed for easy access to key components simplify routine cleaning, maintenance, and changeovers, reducing downtime. Inquire about the availability of spare parts and technical support.
5. Consider Compliance and Supplier Credibility
For food, pharmaceutical, or medical products, ensure the machine meets relevant industry standards (e.g., FDA, GMP, CE). The construction materials (e.g., food-grade stainless steel) and design should facilitate thorough cleaning. Crucially, vet the manufacturer. A supplier with a proven track record, like Packmate with over 30 years of expertise and a 20,000㎡ modern facility, offers reliability, quality assurance, and long-term support, ensuring your investment is protected. Review their project case studies to gauge their experience with similar applications.
Conclusion
Shuttle packaging machines represent a robust and flexible solution for modern production environments. By offering a blend of versatility, precision, and gentle handling, they can significantly enhance packaging quality and operational efficiency. The choice ultimately hinges on a clear understanding of your product requirements, output goals, and the strategic value of partnering with a credible, experienced equipment manufacturer. A well-chosen shuttle system is not just a machine; it’s a long-term asset that drives consistency, reduces waste, and supports brand growth in a competitive marketplace.
Frequently Asked Questions (FAQs)
What is the main difference between a shuttle and a rotary packaging machine?
The core difference lies in the motion. Shuttle machines use a back-and-forth linear motion for forming and sealing, offering excellent registration control and gentle product handling. Rotary machines use a continuous circular motion, typically achieving higher speeds for simpler, standard pouch types. Shuttles are preferred for fragile products and precise graphic alignment.
Can a shuttle machine handle stand-up pouches (doypacks)?
Yes, many advanced shuttle packaging machines are equipped with special forming tools and sealing jaws specifically designed to produce stand-up pouches with gussets. This includes creating the bottom gusset seal that allows the pouch to stand upright.
How difficult is it to changeover pouch sizes on a shuttle machine?
Modern shuttle machines are designed for relatively quick changeovers. The complexity depends on the model. Higher-end machines often feature “tool-less” changeovers where adjustments are made via hand wheels or digital inputs on the HMI, allowing size changes in 15-30 minutes. More basic models may require changing physical parts, taking longer.
What kind of maintenance does a shuttle packaging machine require?
Regular maintenance is crucial for longevity. Daily tasks include cleaning and inspecting sealing jaws, film guides, and cutting blades. Weekly or monthly checks may involve lubricating moving parts, checking belt tensions, and verifying pneumatic systems. Always follow the manufacturer’s specific maintenance schedule outlined in the manual.
Are shuttle machines suitable for liquid or paste products?
Absolutely. Shuttle machines can be configured with specialized liquid pumps (e.g., piston fillers) and nozzles designed to handle viscous products like sauces, creams, or oils without dripping. The key is ensuring the machine has the appropriate filling system and sealing parameters to create a leak-proof pouch.