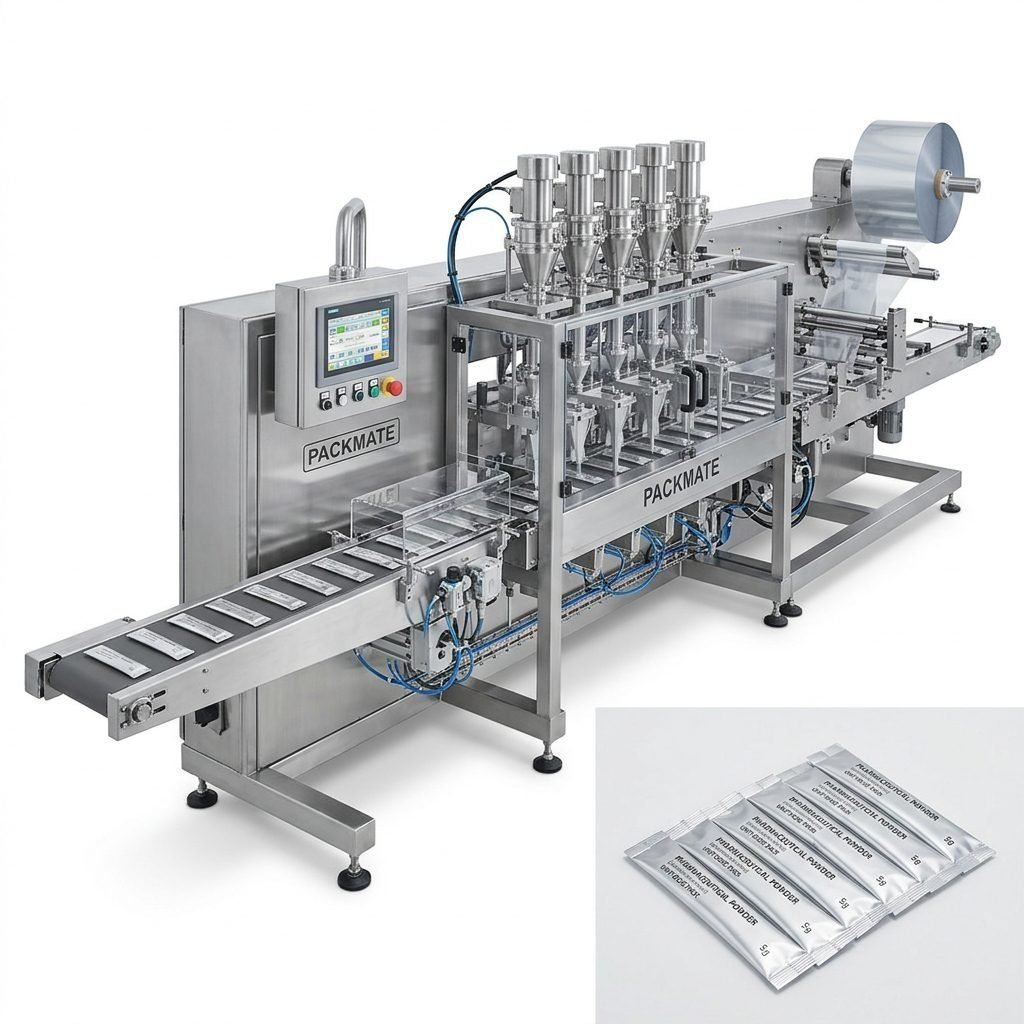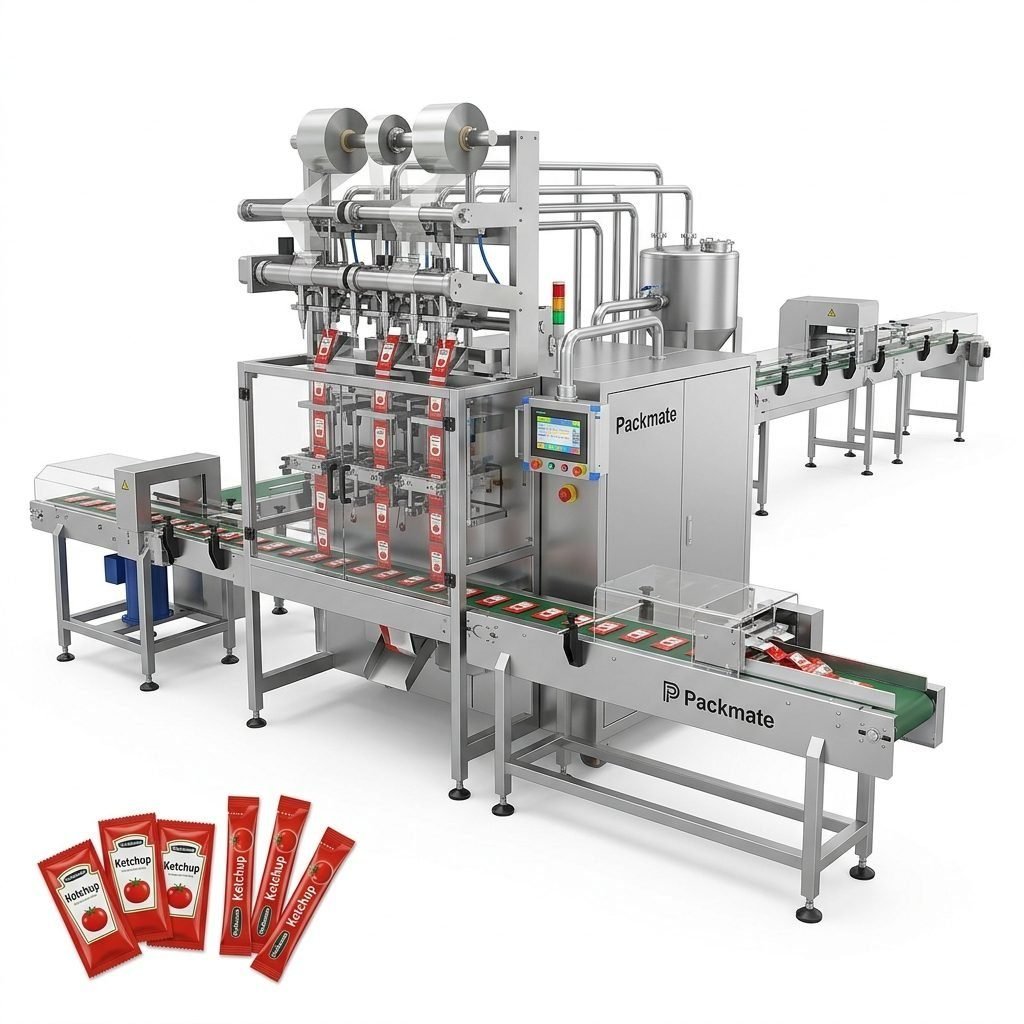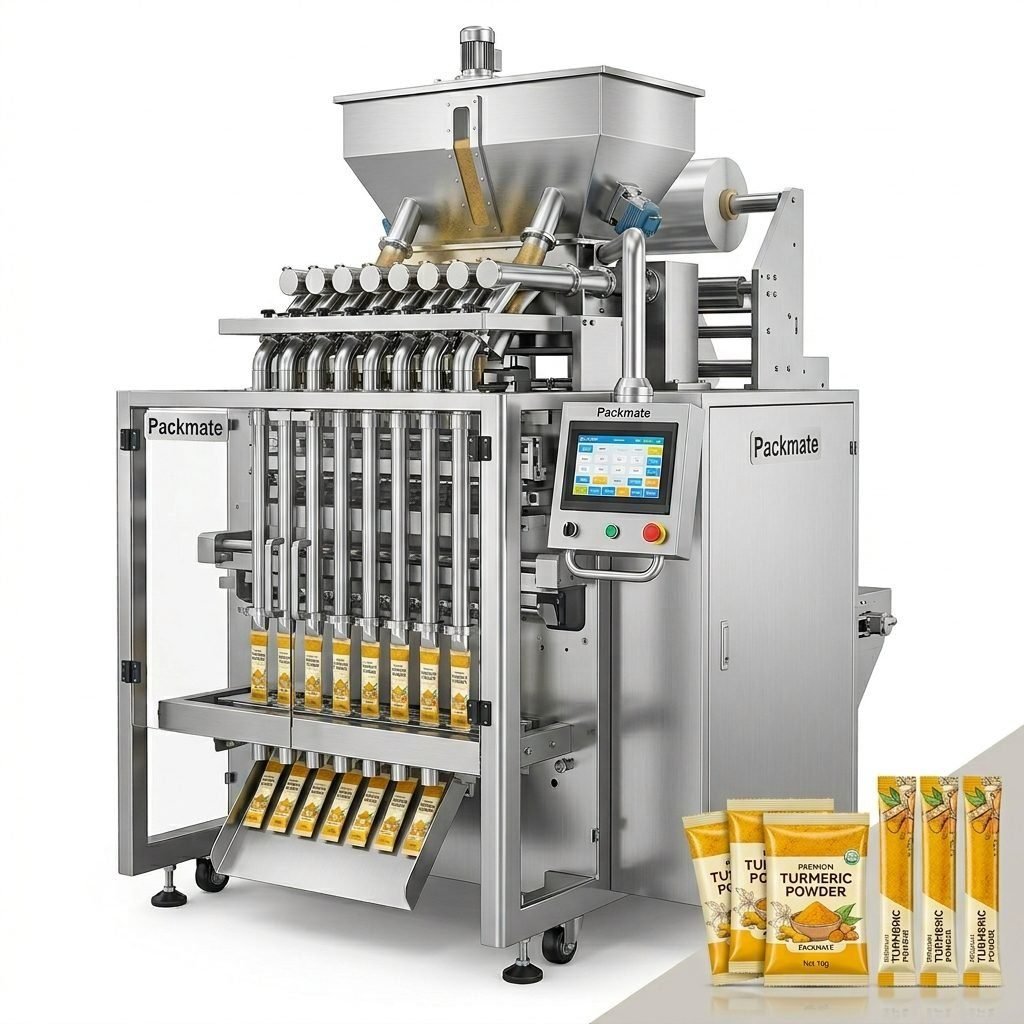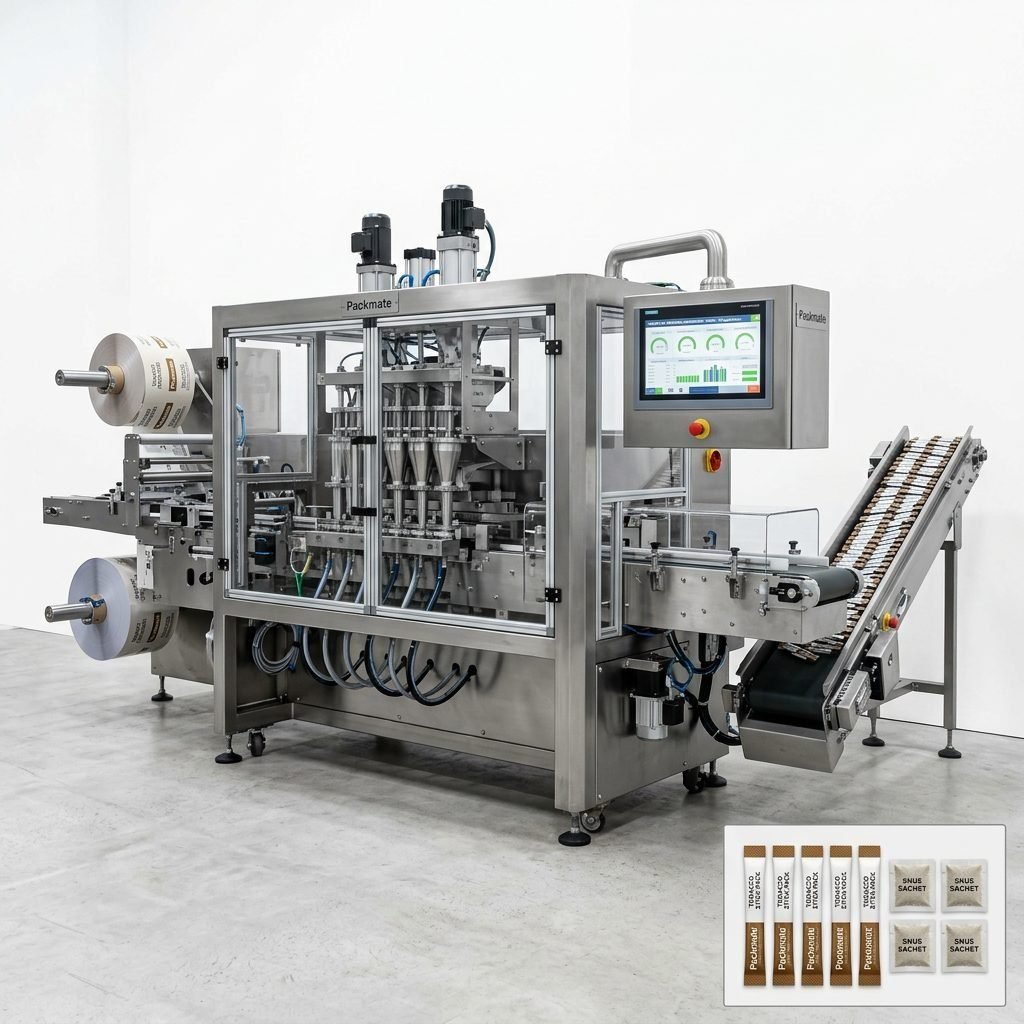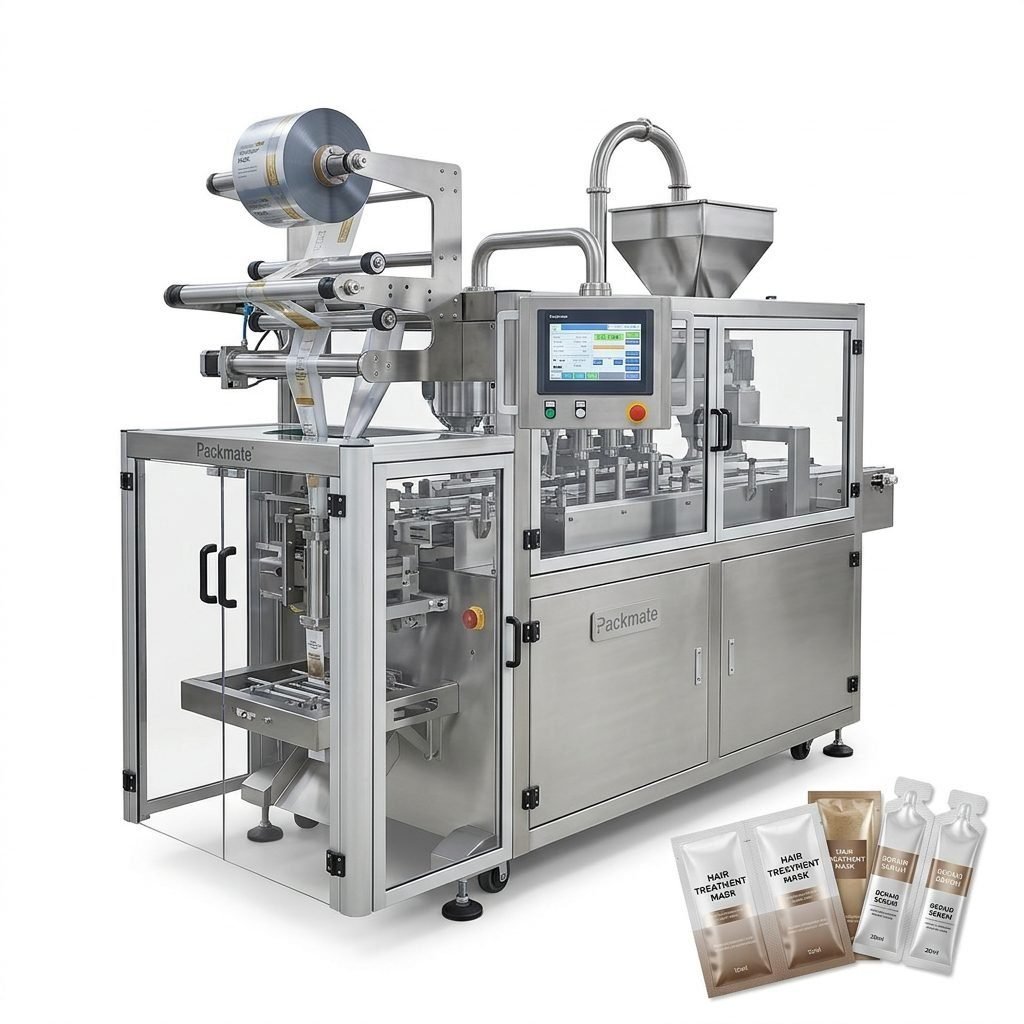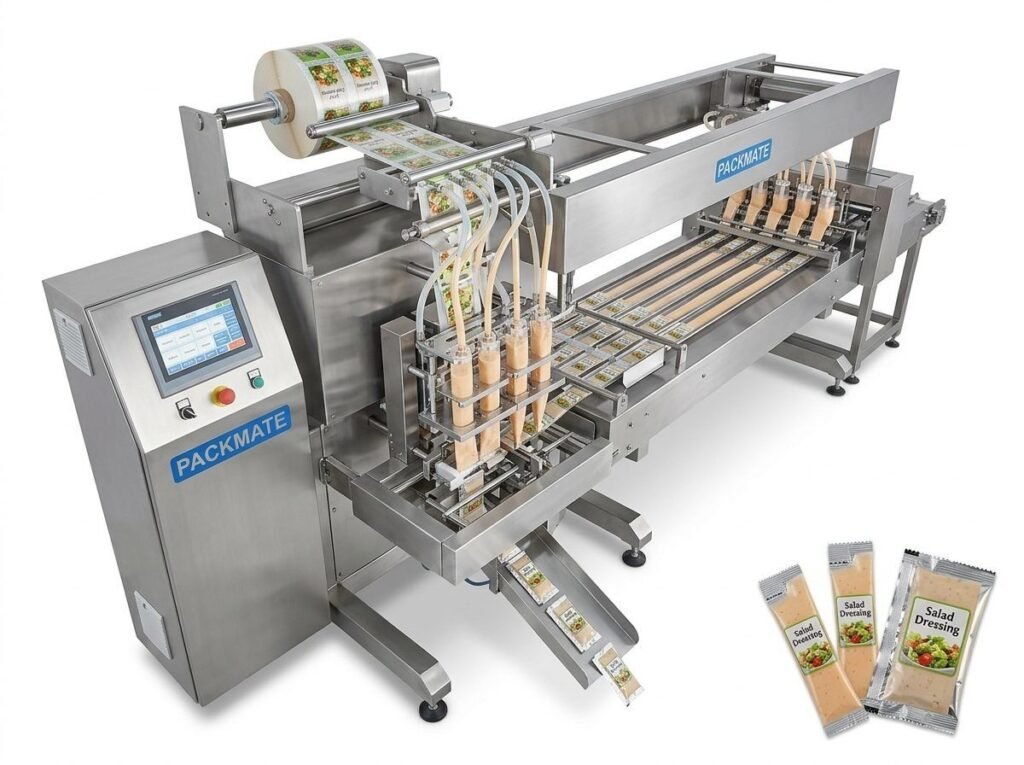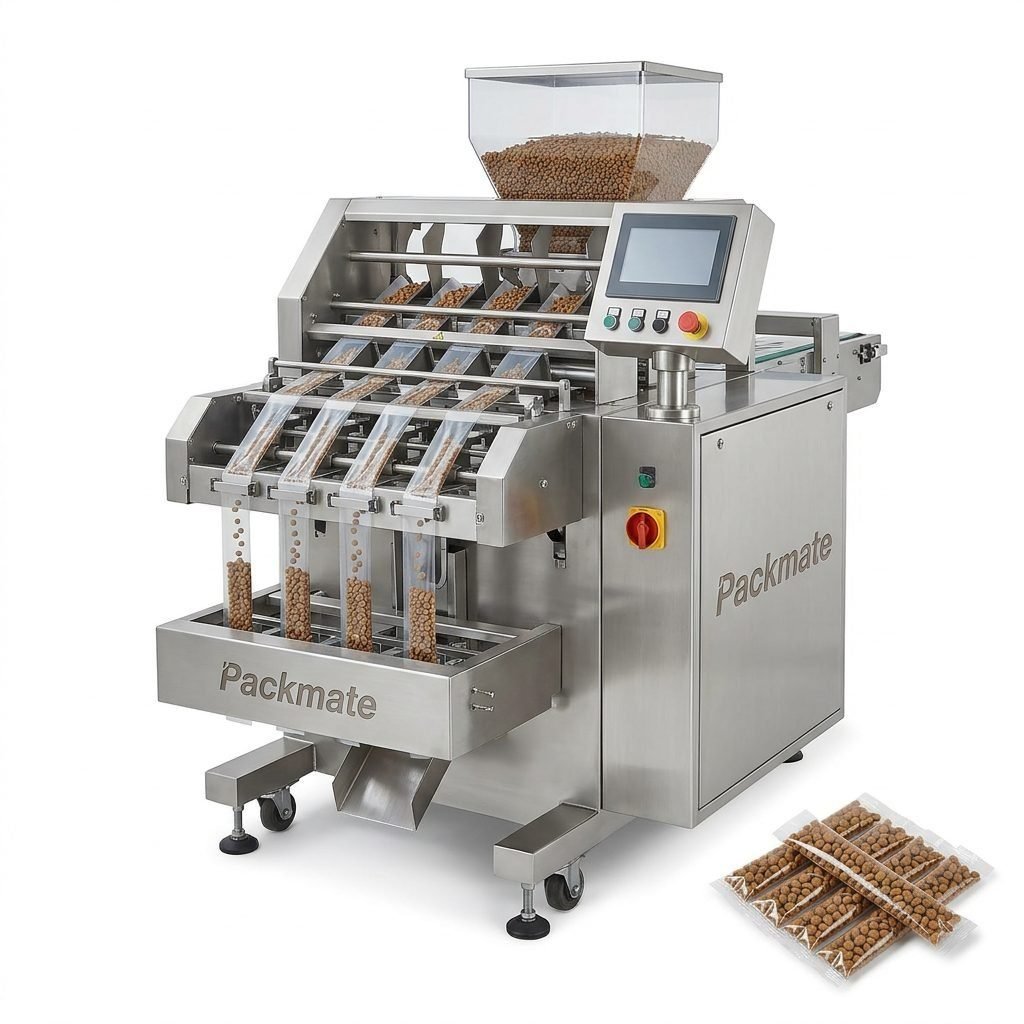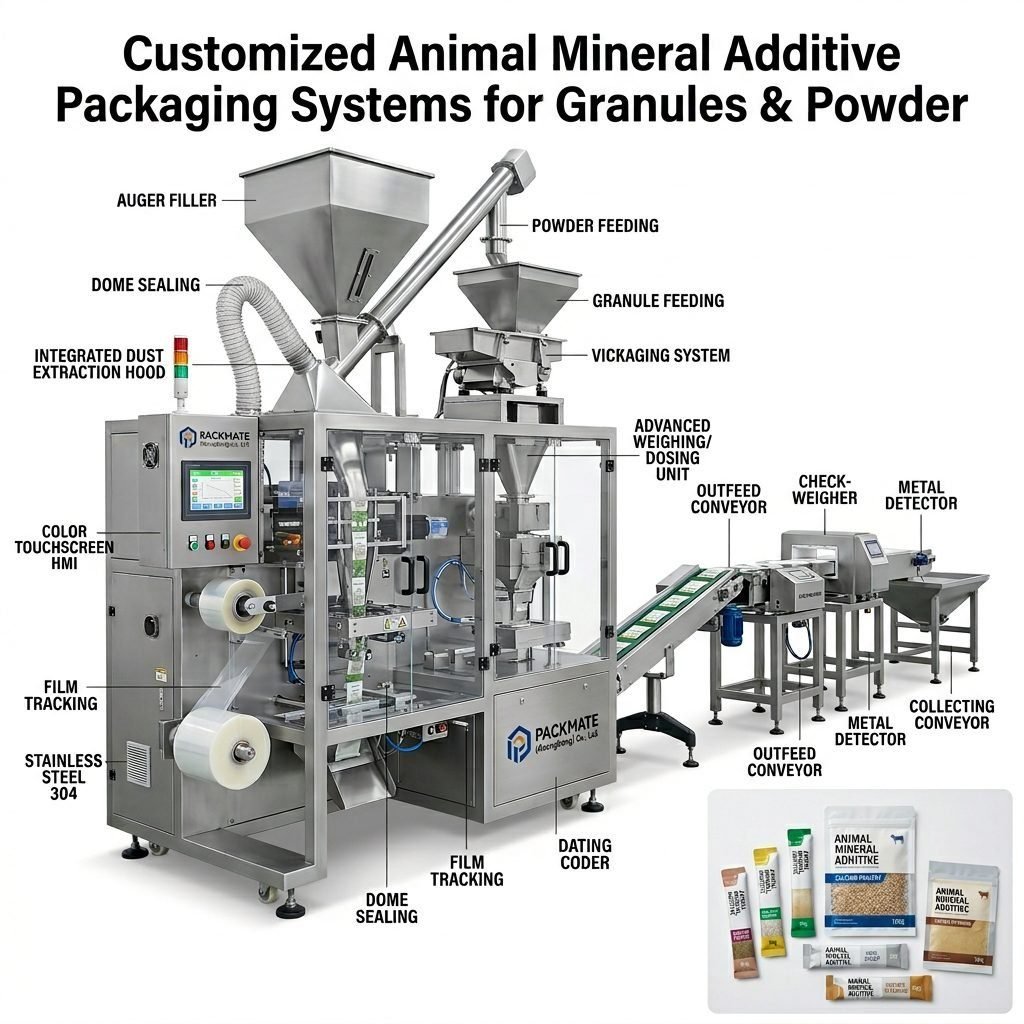
In today’s competitive business landscape, efficiency, reliability, and product presentation are paramount. For industries handling a wide range of products—from food ingredients and pharmaceuticals to health supplements and granular materials—the final packaging stage is critical. Investing in the best case packaging machine solutions is not merely an operational upgrade; it is a strategic decision that impacts productivity, cost management, and brand integrity. This article explores the essential considerations for selecting optimal packaging machinery and how tailored solutions can propel your business forward.
Understanding Your Packaging Needs
Before exploring specific machinery, a thorough assessment of your operational requirements is crucial. Consider the product form—whether you are packaging powders, granules, liquids, or solids. Each type demands different handling, filling, and sealing technologies. Next, evaluate your required output speed and volume. A high-speed production line for consumer goods differs vastly from a smaller, precision-focused line for pharmaceutical samples.
Furthermore, the choice of packaging material—be it laminated films for sachets, paper for stick packs, or pre-formed pouches—directly influences the machine type. Compatibility with your existing production line and future scalability are also vital factors. A solution that grows with your business prevents costly reinvestments down the line.
Key Features of Advanced Case Packaging Machines
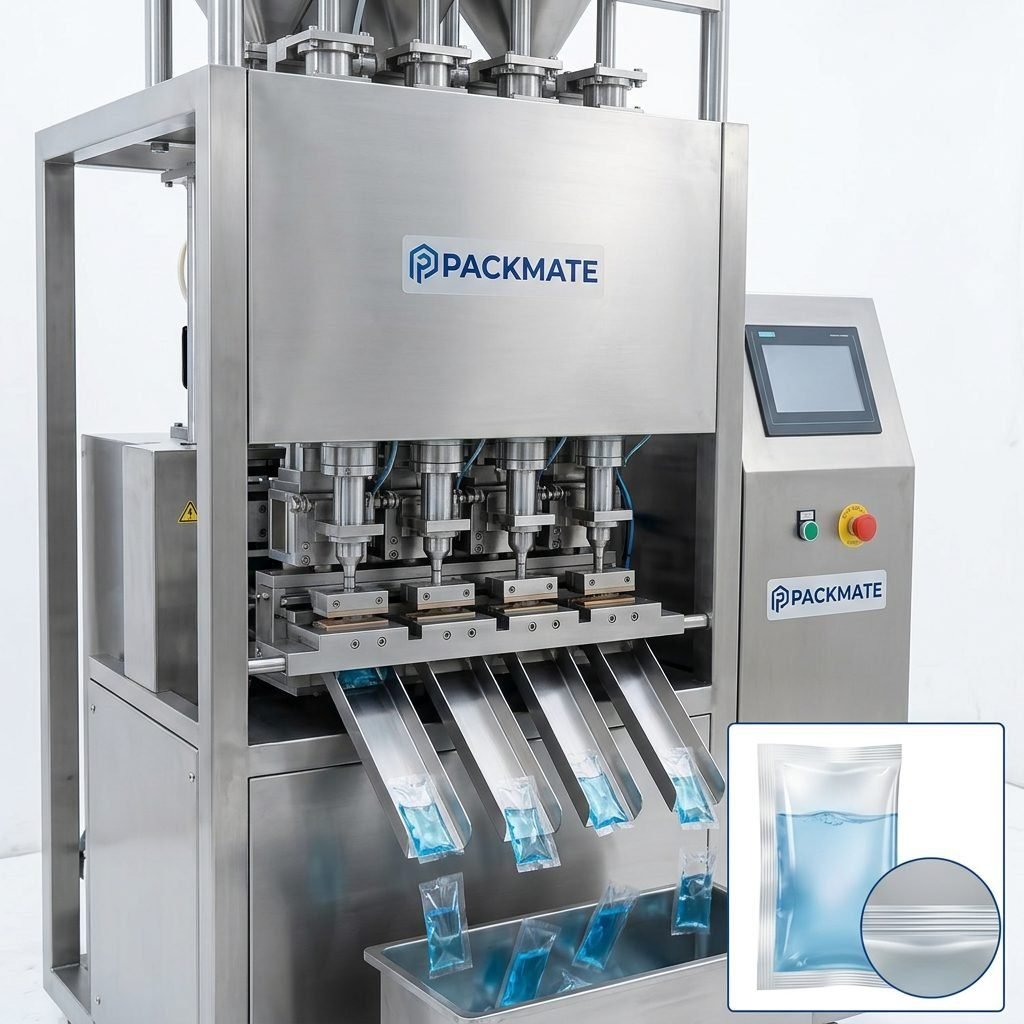
Modern case packaging solutions are marvels of engineering, designed for precision and durability. Look for machines that offer high-speed automation with minimal manual intervention, significantly reducing labor costs and human error. Precision weighing and filling systems are non-negotiable for industries with strict net content regulations, ensuring every package meets exact weight specifications.
Versatility is another hallmark of a superior machine. The ability to handle multiple package sizes and formats with quick changeovers maximizes operational flexibility. Integrated quality control systems, such as checkweighers and metal detectors, provide an additional layer of security and compliance. Finally, robust construction with easy-to-clean surfaces, often made from stainless steel, ensures longevity and meets stringent hygiene standards, especially in food and pharmaceutical applications.
The Role of Turnkey Solutions
For many businesses, especially those expanding or launching new product lines, a piecemeal approach to packaging can create bottlenecks. This is where a complete turnkey packaging solution becomes invaluable. A turnkey line integrates all necessary components—from the initial feeding and weighing to the final case packing—into one seamless, synchronized system.
Partnering with a manufacturer that provides turnkey services, like Packmate Machinery, means you get a single point of responsibility for design, installation, commissioning, and training. This holistic approach minimizes integration headaches, accelerates time-to-market, and ensures all components are optimized to work together for peak efficiency and output quality.
Benefits of Optimizing Your Packaging Line
Upgrading to a best-in-class case packaging machine delivers tangible returns across your operation. The most immediate impact is on productivity and throughput. Automated lines can operate continuously at high speeds, dramatically increasing your daily output. This scalability is essential for meeting growing demand or seasonal spikes.
Enhanced product protection and shelf appeal are direct benefits. Consistent, secure seals prevent contamination and spoilage, while precise packaging creates a professional, attractive product that stands out on retail shelves. Moreover, modern machines are designed for material efficiency, reducing film waste and optimizing raw material usage, which contributes directly to a healthier bottom line and more sustainable operations.
Choosing the Right Partner: Beyond the Machine
Selecting the best case packaging machine is only half the battle. The manufacturer you choose as a partner is equally critical. Look for a company with a proven track record and deep industry expertise. For instance, with over 30 years of experience, Packmate Machinery has evolved from a specialized workshop to a leader providing intelligent packaging equipment for global markets.
A reliable partner offers comprehensive after-sales support, including readily available spare parts, prompt technical service, and operator training. They should understand global standards and certifications, ensuring their machines help you comply with regional regulations. The ability to provide customized modifications to standard models to fit your unique product or process is the mark of a truly collaborative supplier.
Future-Proofing Your Investment
Technology in packaging is advancing rapidly. The best case packaging machine solutions today are built with connectivity and Industry 4.0 principles in mind. Features like IoT-enabled monitoring, predictive maintenance alerts, and data analytics capabilities allow for smarter production management. These machines can integrate with factory-wide management systems, providing real-time data on output, efficiency, and downtime.
Investing in a modular and upgradeable platform ensures your packaging line can adapt to new materials, incorporate future technologies like advanced vision systems, or expand its functionality without requiring a complete replacement. This forward-thinking approach protects your capital investment and keeps your operations at the competitive forefront.
Ultimately, the quest for the best case packaging machine solution is a strategic investment in your business’s core operational capabilities. It enhances efficiency, ensures product quality, and supports brand growth. By carefully evaluating your needs, prioritizing key features like speed and versatility, and partnering with an experienced and supportive manufacturer, you can implement a solution that delivers immediate benefits and scales for future success.
Frequently Asked Questions (FAQ)
1. What factors are most important when choosing a case packaging machine?
The primary factors include your product type (powder, granule, liquid), required production speed, packaging material, and the level of automation needed. Compliance with industry-specific hygiene or safety standards is also critical.
2. Can one machine handle different package sizes or products?
Many modern machines are designed for versatility. Look for models with quick-changeover features that allow you to switch between different package formats or sizes with minimal downtime and tooling adjustments.
3. How does a turnkey packaging line differ from buying individual machines?
A turnkey line is a complete, pre-integrated system supplied by a single vendor. It includes all necessary equipment, from feeding to final packaging, and is commissioned as a whole unit. This approach ensures compatibility, reduces project complexity, and often results in faster overall installation and optimization compared to sourcing machines separately.
4. What kind of after-sales support should I expect?
Comprehensive support includes installation supervision, detailed operator and maintenance training, readily available spare parts, remote technical assistance, and access to service engineers for on-site repairs if necessary. A strong global service network is essential for international operations.
5. How can I ensure the machine meets food or pharmaceutical safety standards?
Choose machinery constructed with appropriate materials, such as food-grade stainless steel for contact parts. Ensure the design allows for easy cleaning and sanitization (CIP/SIP capabilities where required). Reputable manufacturers will design machines in compliance with relevant standards (e.g., GMP, FDA guidelines) and can provide necessary documentation and certifications.