The global packaging machinery industry is a dynamic and competitive landscape, where innovation, reliability, and comprehensive solutions separate the market leaders from the rest. For businesses in the food, pharmaceutical, and health sectors, selecting the right equipment supplier is a critical decision that impacts operational efficiency, product quality, and ultimately, profitability. This exploration delves into the qualities that define top packaging machinery companies and leading industry suppliers, highlighting the expertise required to deliver intelligent, turnkey packaging solutions for modern production demands.
Defining Excellence in Packaging Machinery
Top-tier packaging machinery companies are characterized by more than just a product catalog. They are partners in production, offering a blend of advanced engineering, deep industry knowledge, and unwavering support. These suppliers understand that packaging is the final, critical touchpoint before a product reaches the consumer, making precision and consistency non-negotiable. They invest heavily in research and development to create machines that are not only fast and efficient but also adaptable, hygienic, and increasingly intelligent with integrated IoT capabilities for data-driven operations.
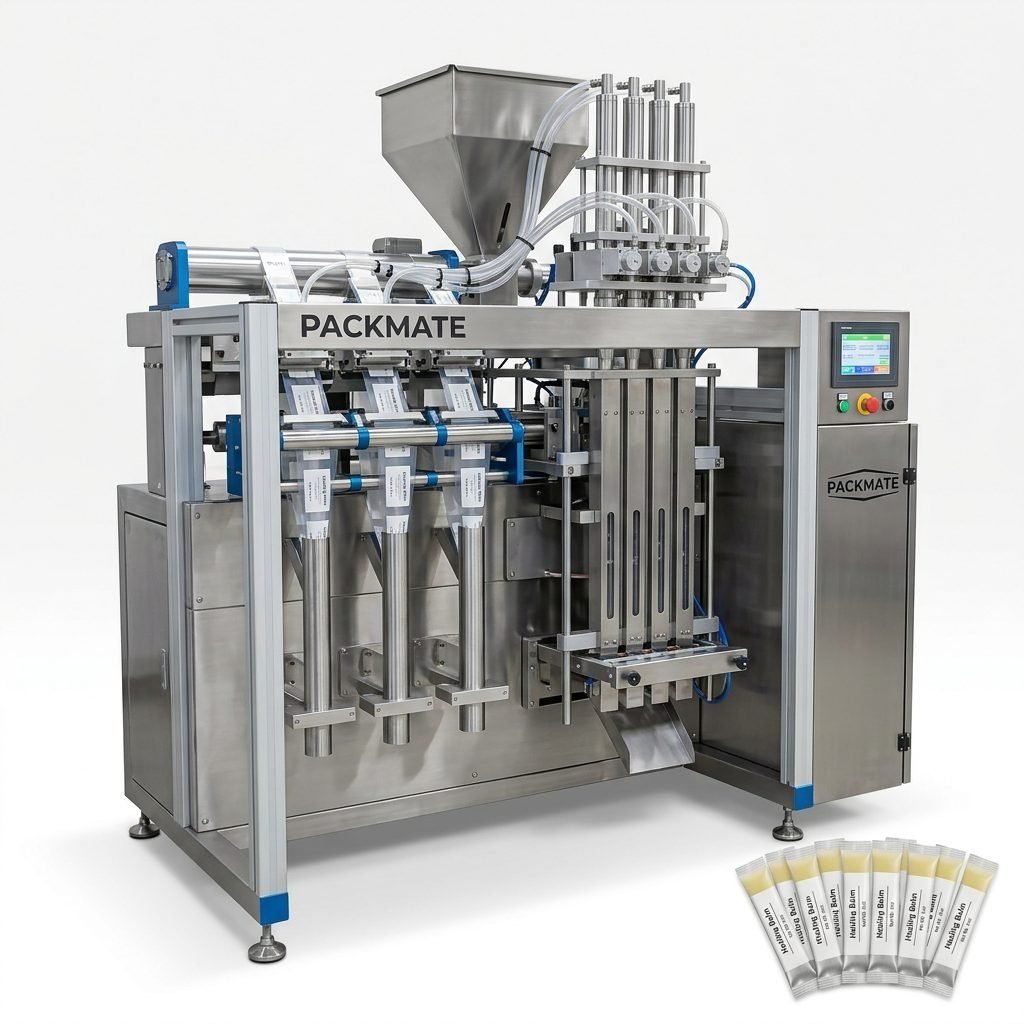
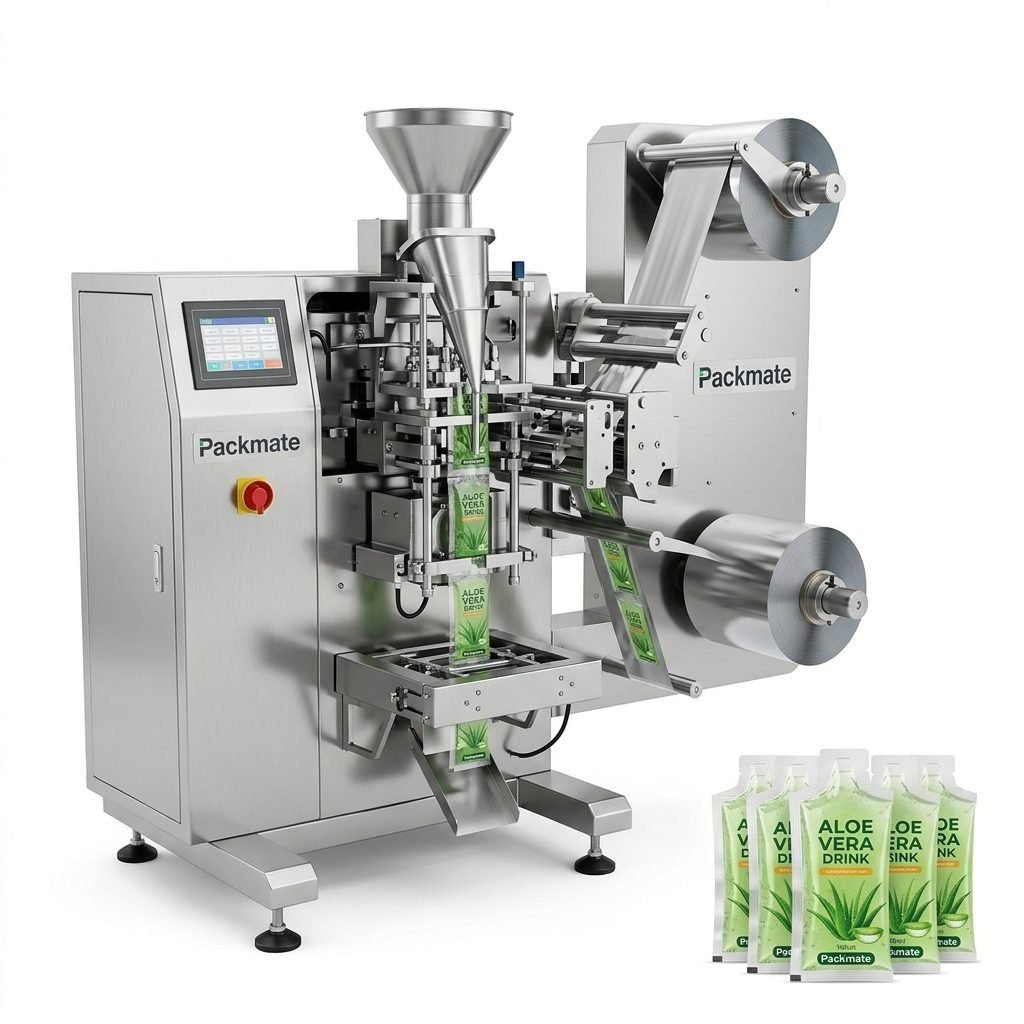
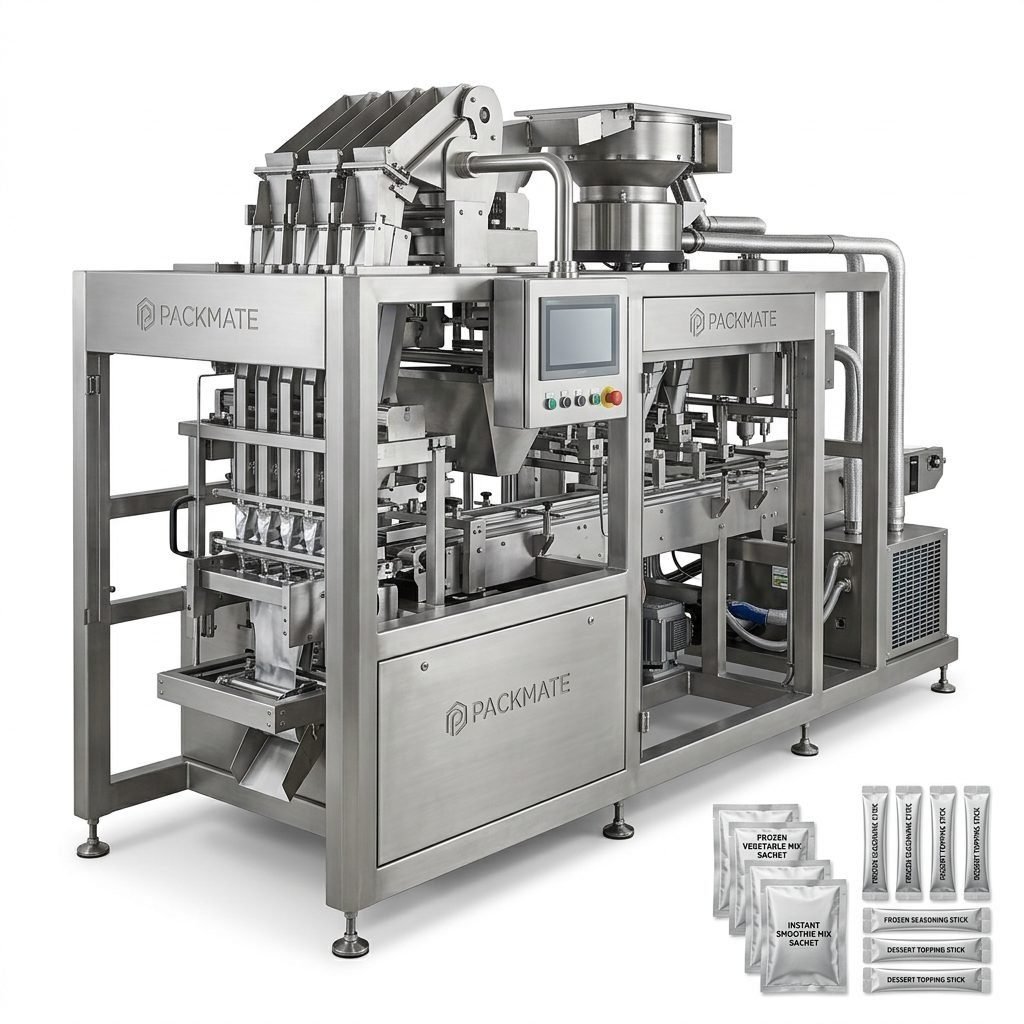
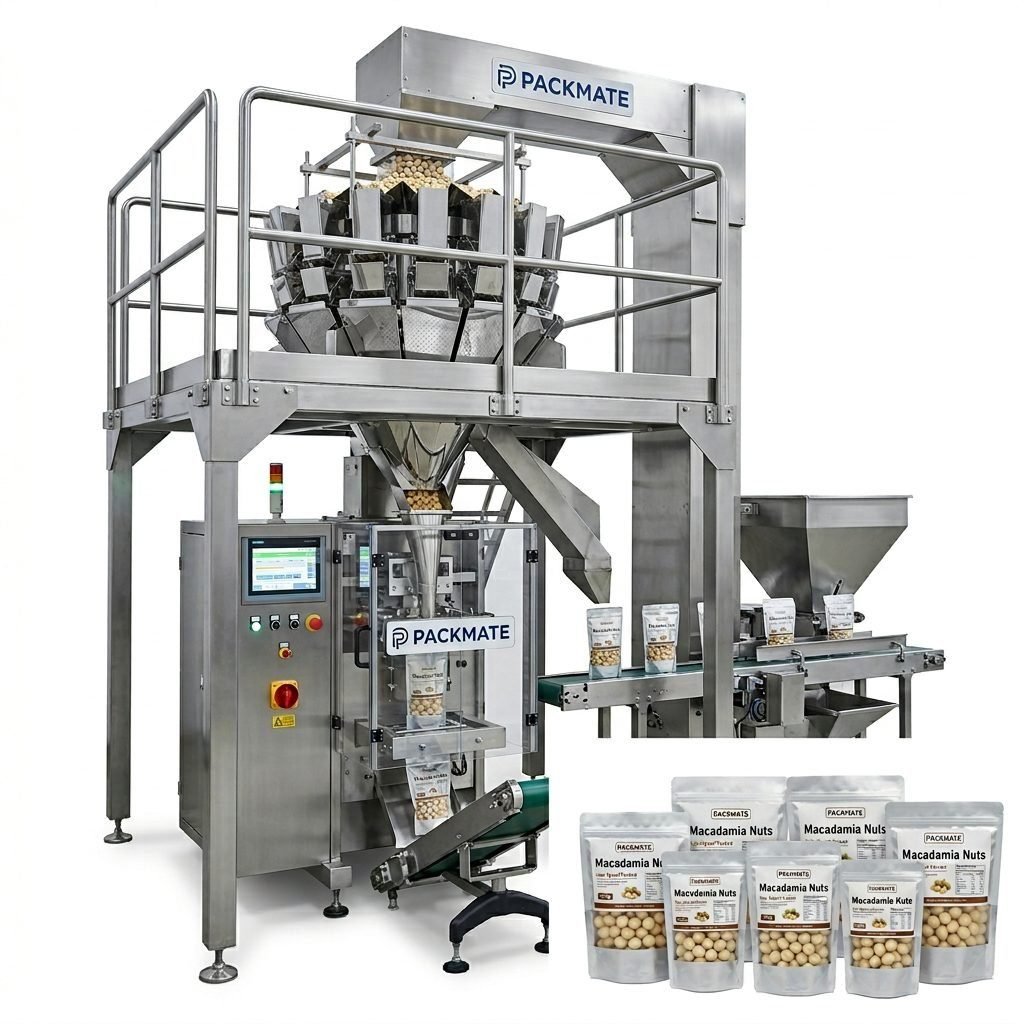
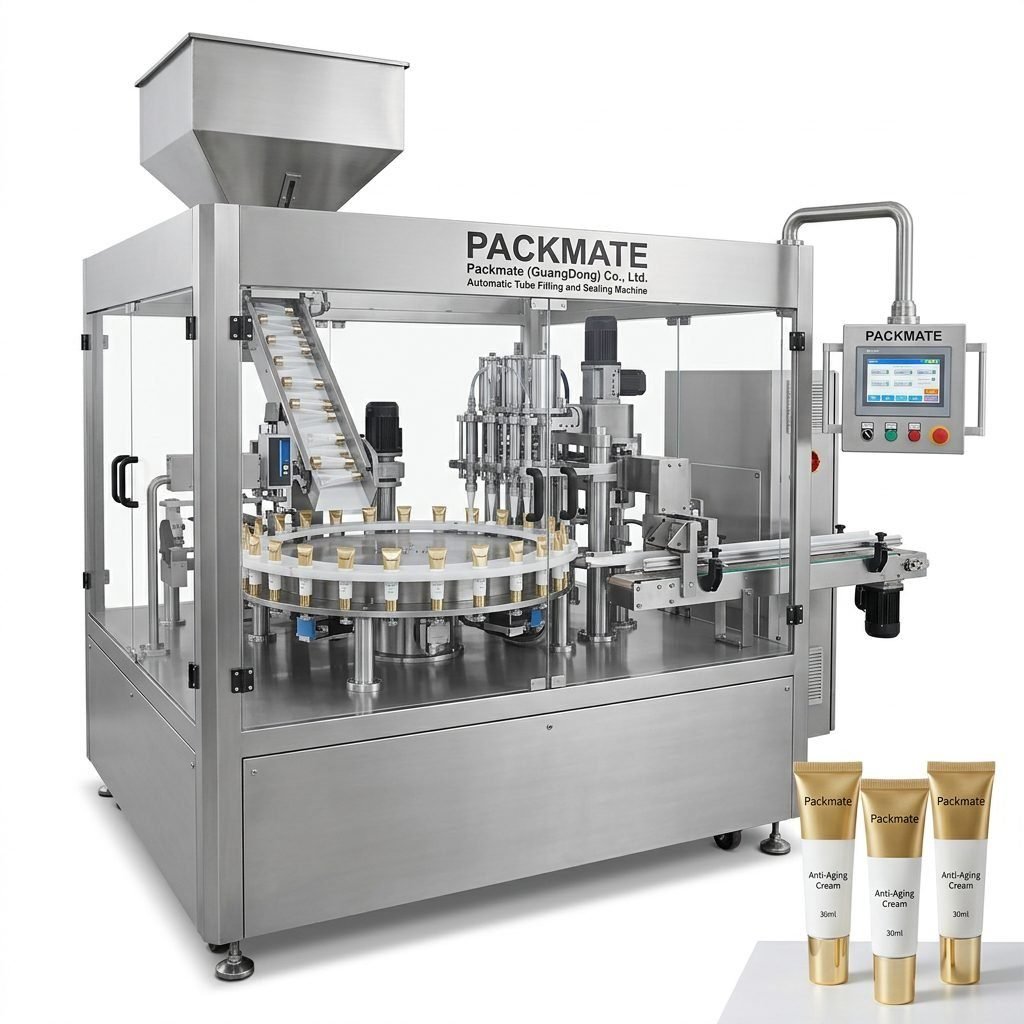
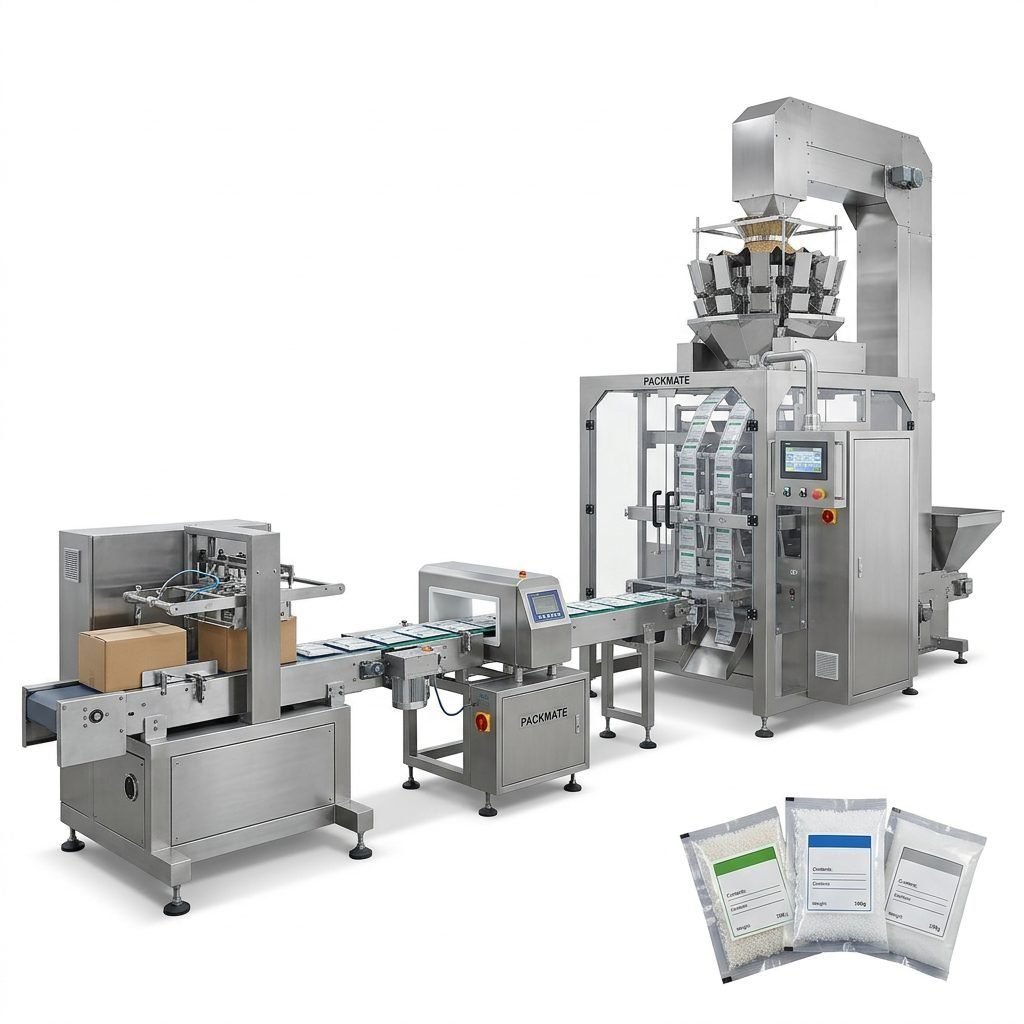
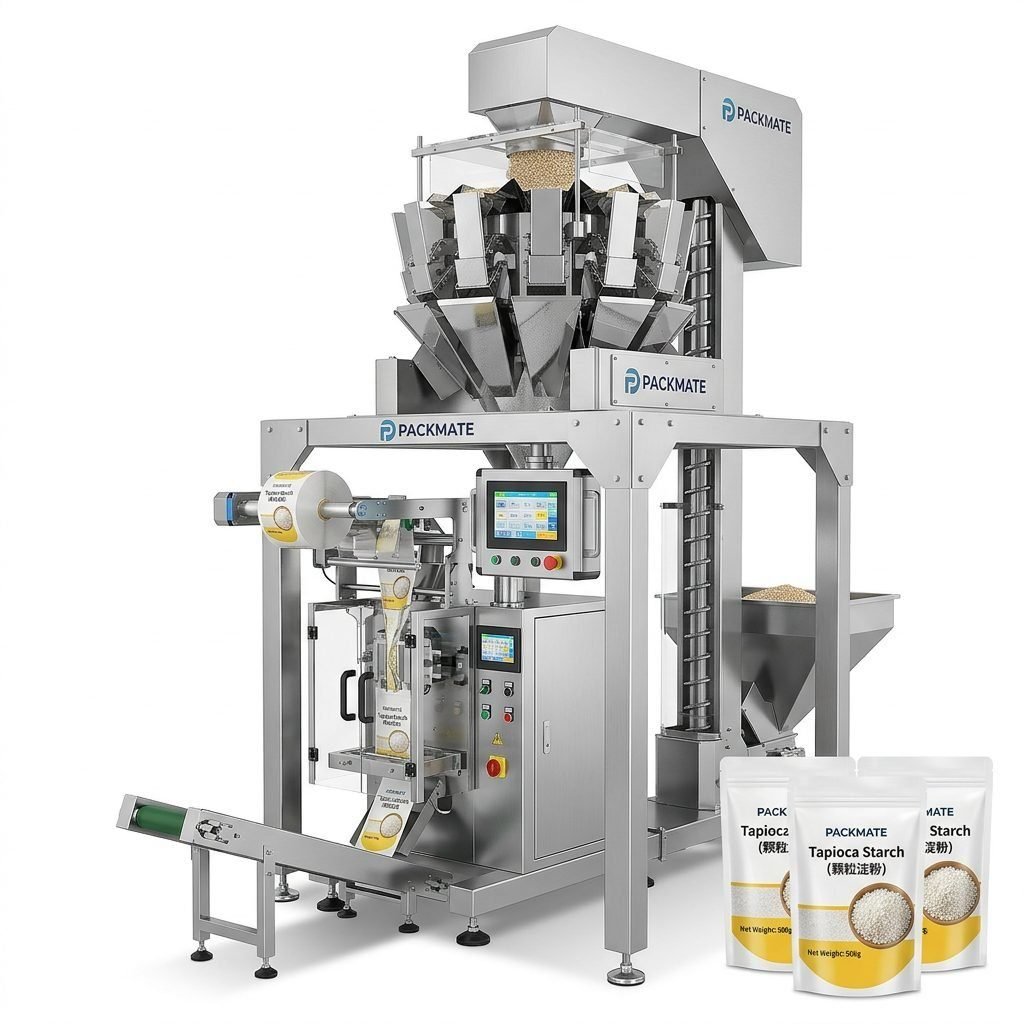
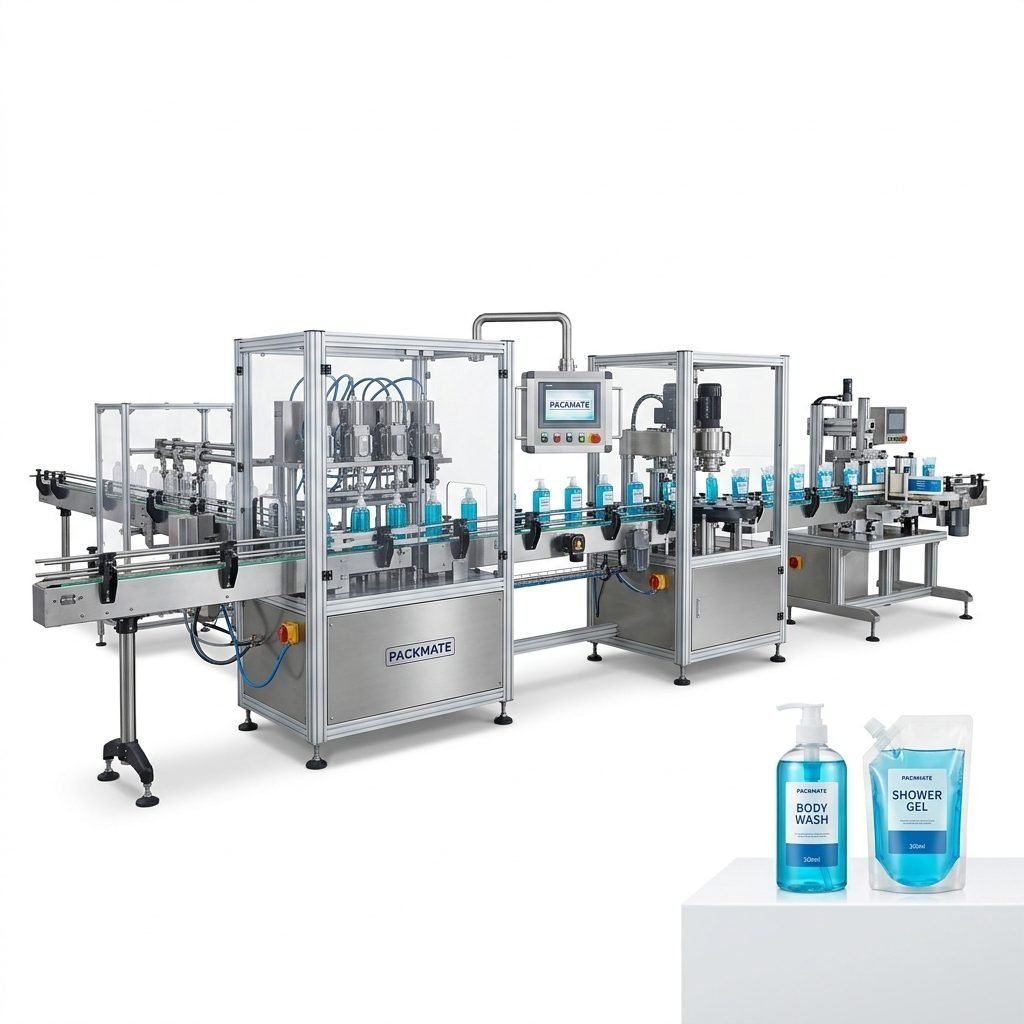
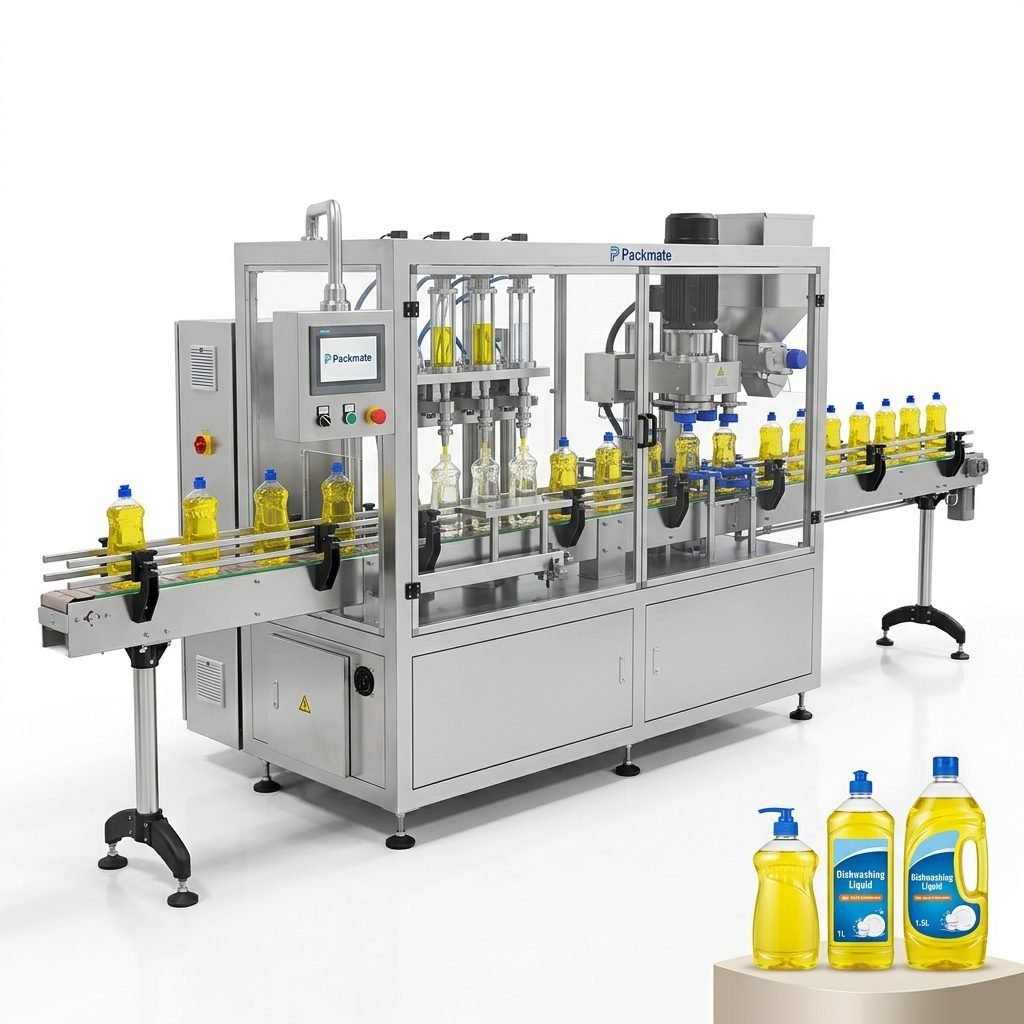
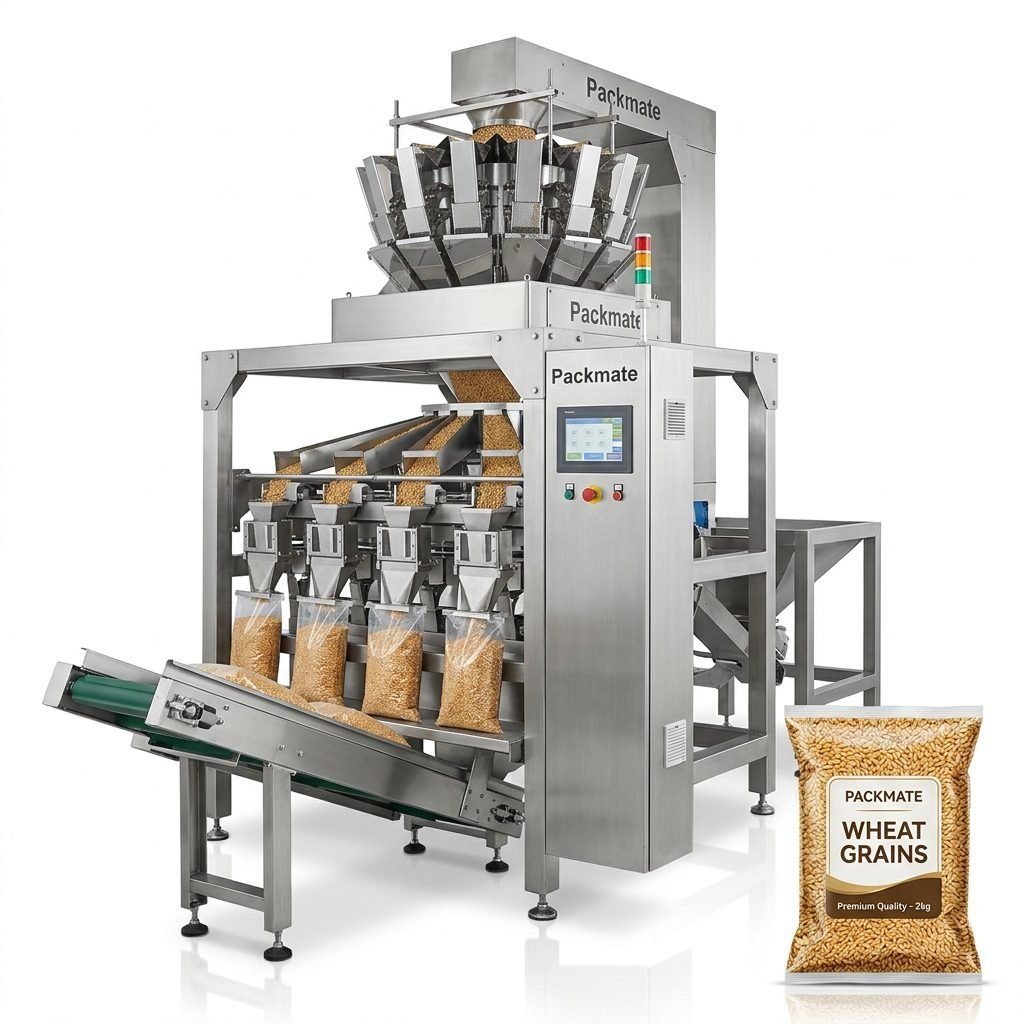
A leading supplier’s portfolio typically spans a wide range of applications, from handling delicate powders and granules to managing viscous liquids. Key equipment lines include sophisticated Sachet & Stick Pack Machines for single-serve portions, robust Bag & Pouch Packaging Machines for retail, and complete Filling & Packaging Lines that integrate weighing, filling, and sealing into one seamless process. The ability to provide such comprehensive systems is a hallmark of industry leadership.
The Pillars of a Leading Supplier
Several core pillars support the reputation of a leading packaging machinery company. First is technological prowess – the continuous innovation in servo-motor control, touch-screen HMIs, and quick-changeover mechanisms that minimize downtime. Second is manufacturing scale and quality control. Operating from a modern facility, like Packmate’s 20,000㎡ factory, allows for vertical integration, stringent testing, and the capacity to handle large, custom orders while maintaining quality. Third is global experience and support. A true industry leader has a proven track record of installing and servicing machines worldwide, understanding diverse market regulations and client needs.
Innovation Driven by Experience
The journey to becoming a top supplier is often rooted in decades of focused expertise. Consider a company like Packmate Machinery, whose story began over 30 years ago with a founder’s passion for automation. From humble beginnings in a small workshop, solving persistent technical challenges, the company evolved into a formal entity by 2003. This long-term dedication translates into profound practical knowledge. Engineers with 20+ years of experience design machines that are not just theoretically sound but are rugged, reliable, and optimized for real-world factory conditions. This deep-seated experience is invaluable when developing specialized equipment, such as machines for the nuanced demands of the snus and nicotine pouch market.
Commitment to Turnkey Solutions
Today’s manufacturers seek more than a machine; they seek a solution. Leading suppliers have shifted from being mere equipment vendors to becoming providers of complete turnkey projects. This means taking responsibility from initial concept and factory layout planning, through machine design and manufacturing, to installation, commissioning, and operator training. They offer ancillary equipment—like cartoners, case packers, and checkweighers—to create a fully synchronized production line. This holistic approach, centered on the client’s end-to-end packaging process, significantly reduces project complexity and risk for the buyer, ensuring a smoother path to operational readiness.
The Role of Customization and Flexibility
In an era of product diversification and short production runs, flexibility is key. Top packaging machinery companies excel at offering customizable solutions. Whether it’s modifying a standard machine to handle a unique pouch shape, integrating specific filling technology for abrasive materials, or creating a multi-lane system for high-volume output, the ability to tailor equipment is crucial. This flexibility extends to software, with programmable logic controllers (PLCs) that can store recipes for dozens of products, allowing for quick changeovers that enhance overall equipment effectiveness (OEE).
Sustainability and Efficiency
Leading industry suppliers are also at the forefront of sustainable packaging trends. They engineer machines that optimize material usage, reduce film waste through precise sealing controls, and support the use of recyclable or compostable packaging materials. Energy efficiency is another critical focus, with newer generations of machines designed to consume less power without compromising speed. By helping clients reduce their material footprint and energy costs, these companies add significant long-term value beyond the initial purchase.
Ultimately, partnering with a top packaging machinery company is an investment in future-proofing your production capabilities. It provides access to robust technology, expert support, and a partnership geared towards solving evolving packaging challenges. As consumer preferences and regulatory landscapes change, having a supplier that can adapt and innovate alongside your business becomes an indispensable competitive advantage.
Frequently Asked Questions (FAQs)
What factors should I prioritize when choosing a packaging machinery supplier?
Focus on the supplier’s industry experience, especially with your specific product type (powders, liquids, etc.). Evaluate their technical support and spare parts availability, the flexibility and customization options of their machines, and their ability to provide a complete, integrated line rather than just a single unit. Reviewing their project case studies can offer practical insights.
How important is after-sales service from the machinery manufacturer?
It is critically important. Reliable after-sales service, including readily available spare parts, remote troubleshooting, and on-site technician support, ensures maximum machine uptime. It directly impacts your return on investment and long-term operational stability.
Can packaging machines handle different packaging materials?
Yes, most modern machines from leading suppliers are designed with material flexibility in mind. However, it is essential to discuss your specific materials (e.g., laminate structures, recyclable films) with the supplier during the planning phase. They can configure sealing jaws, tension controls, and film feeding systems to ensure compatibility and optimal performance.
What is the typical lead time for a custom packaging line?
Lead times vary significantly based on complexity, customization level, and current production schedules. For a standard machine, it might be 2-4 months. For a fully custom, multi-machine turnkey line, it could take 6 months or more. A reputable supplier will provide a detailed project timeline upfront.
Do suppliers offer training for our operators and maintenance staff?
Yes, comprehensive training is a standard part of the service from top companies. This usually includes detailed operational training during commissioning at your facility and often covers basic maintenance procedures to empower your team and ensure safe, efficient machine operation.