In today’s fast-paced manufacturing landscape, finding the right shrink packaging equipment supplier is crucial for operational success. The market demands solutions that are not only reliable and efficient but also adaptable to evolving production needs. This article explores the key attributes of top-tier suppliers and highlights how companies like Packmate Machinery deliver exceptional value through innovation, quality, and comprehensive service.
What Defines a Reliable Shrink Packaging Equipment Supplier?
A reliable supplier is characterized by consistent product performance, robust after-sales support, and a proven track record. Equipment must operate with minimal downtime, ensuring continuous production flow. Suppliers should offer comprehensive warranties, readily available spare parts, and responsive technical assistance. This reliability translates directly to reduced operational risk and enhanced productivity for your business.
Beyond the machine itself, reliability is built on transparent communication, accurate delivery timelines, and a deep understanding of client-specific challenges. The best suppliers act as partners, invested in your long-term success.
Core Components of Efficient Packaging Solutions
Efficiency in shrink packaging is multi-faceted. It encompasses speed, material usage optimization, energy consumption, and labor requirements. Modern efficient solutions leverage advanced servo technology for precise motion control, intelligent heat management systems to reduce energy waste, and user-friendly HMIs (Human-Machine Interfaces) for quick changeovers and minimal operator training.
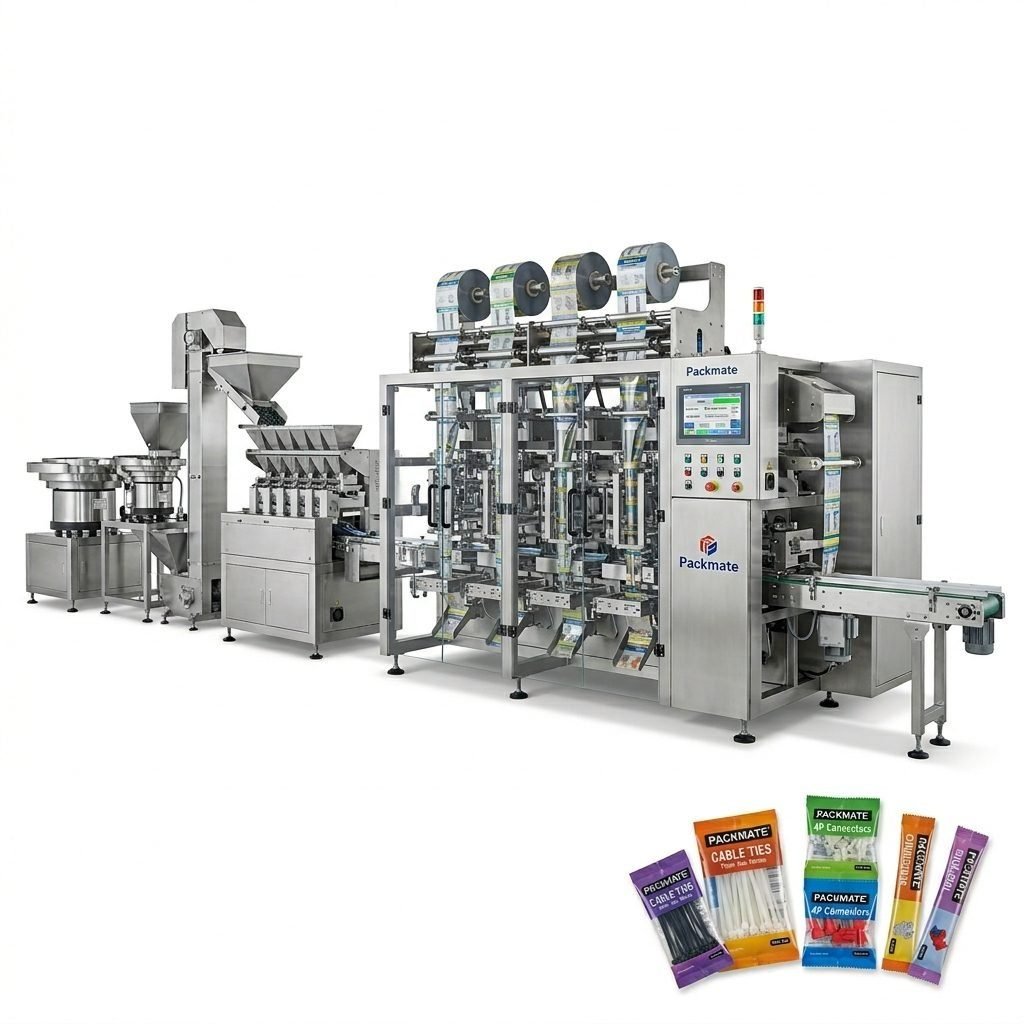
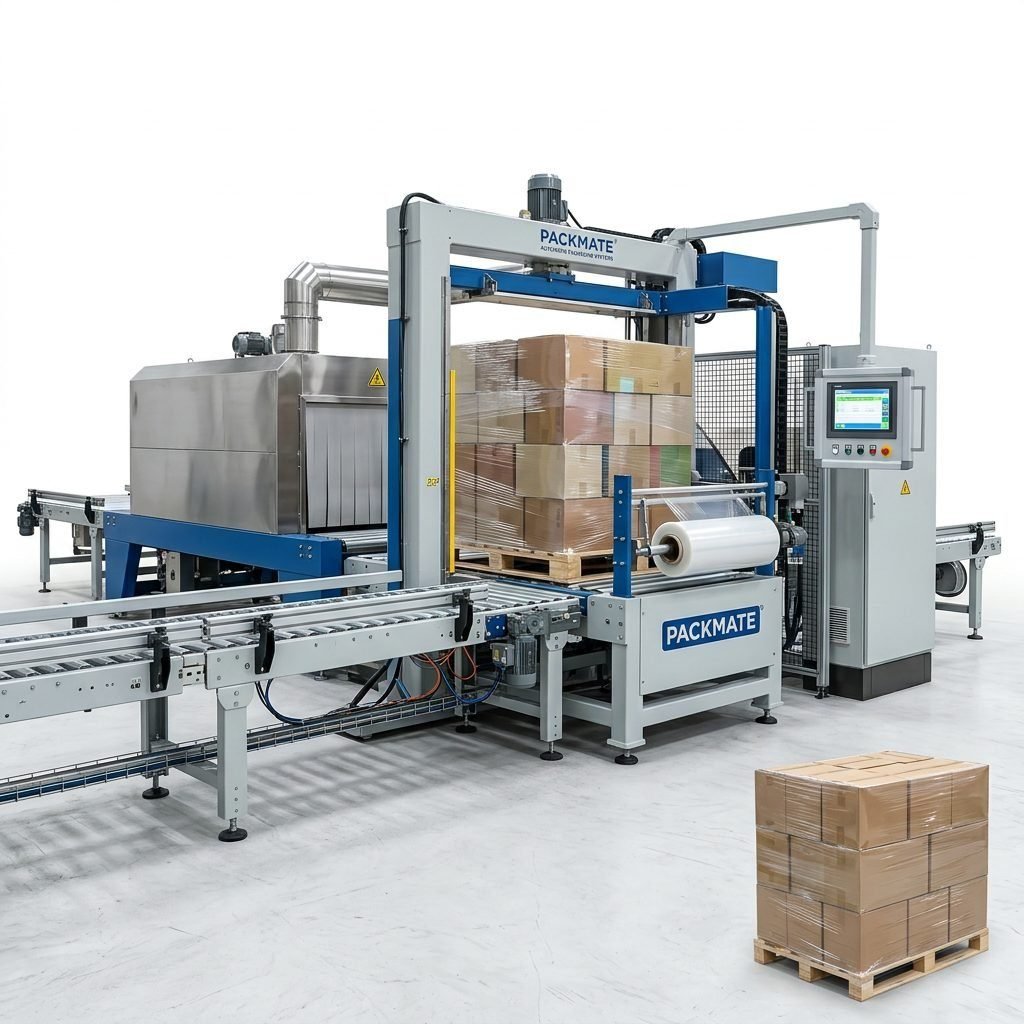
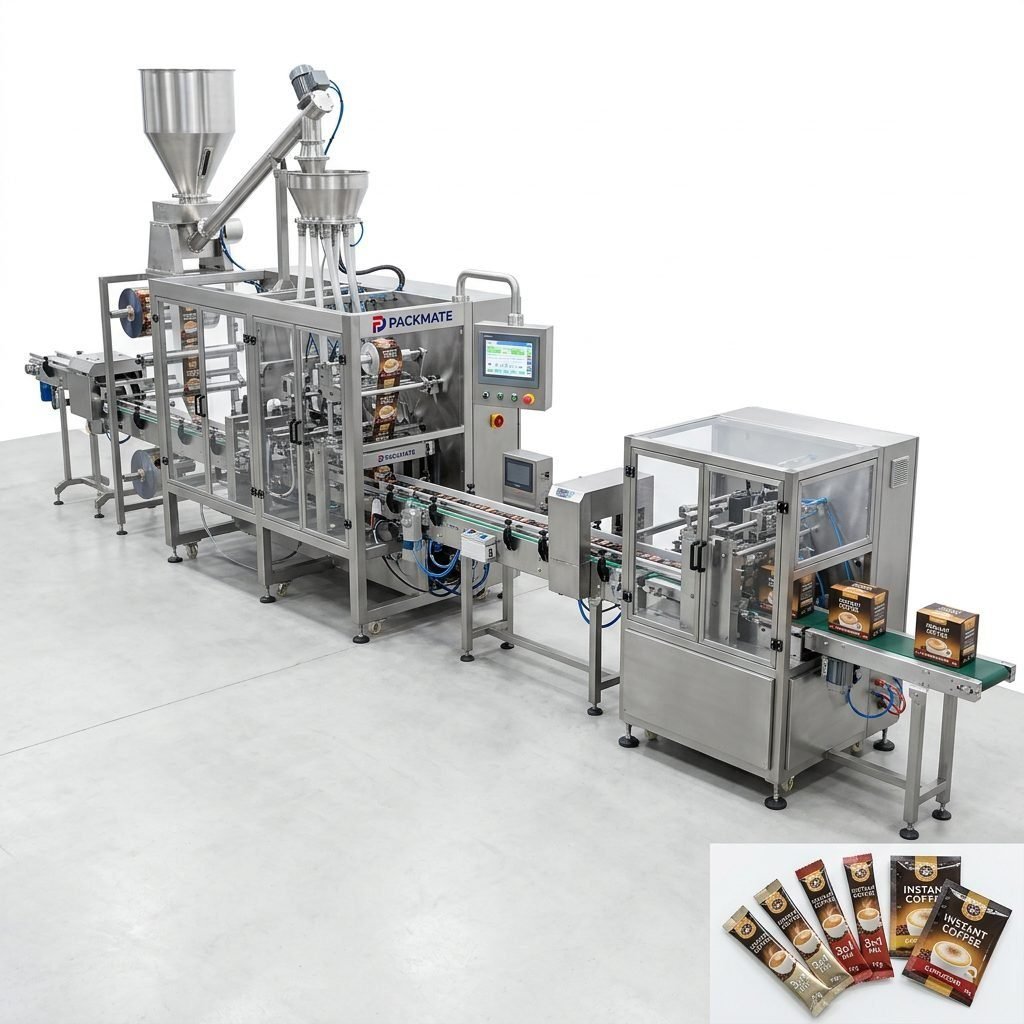
Integration capabilities are also vital. Equipment should seamlessly connect with upstream filling systems and downstream case packing or palletizing lines. This holistic approach to efficiency, often provided through complete filling and packaging lines, eliminates bottlenecks and maximizes overall equipment effectiveness (OEE).
The Packmate Machinery Advantage: A Case Study in Excellence
With over 30 years of expertise, Packmate Machinery exemplifies the qualities of a top supplier. Operating from a modern 20,000㎡ facility in Guangdong, China, the company has evolved from a visionary workshop in 1993 into a global provider of intelligent packaging solutions. Their journey underscores a commitment to innovation, quality, and collaborative partnership.
Key Strengths of a Leading Supplier
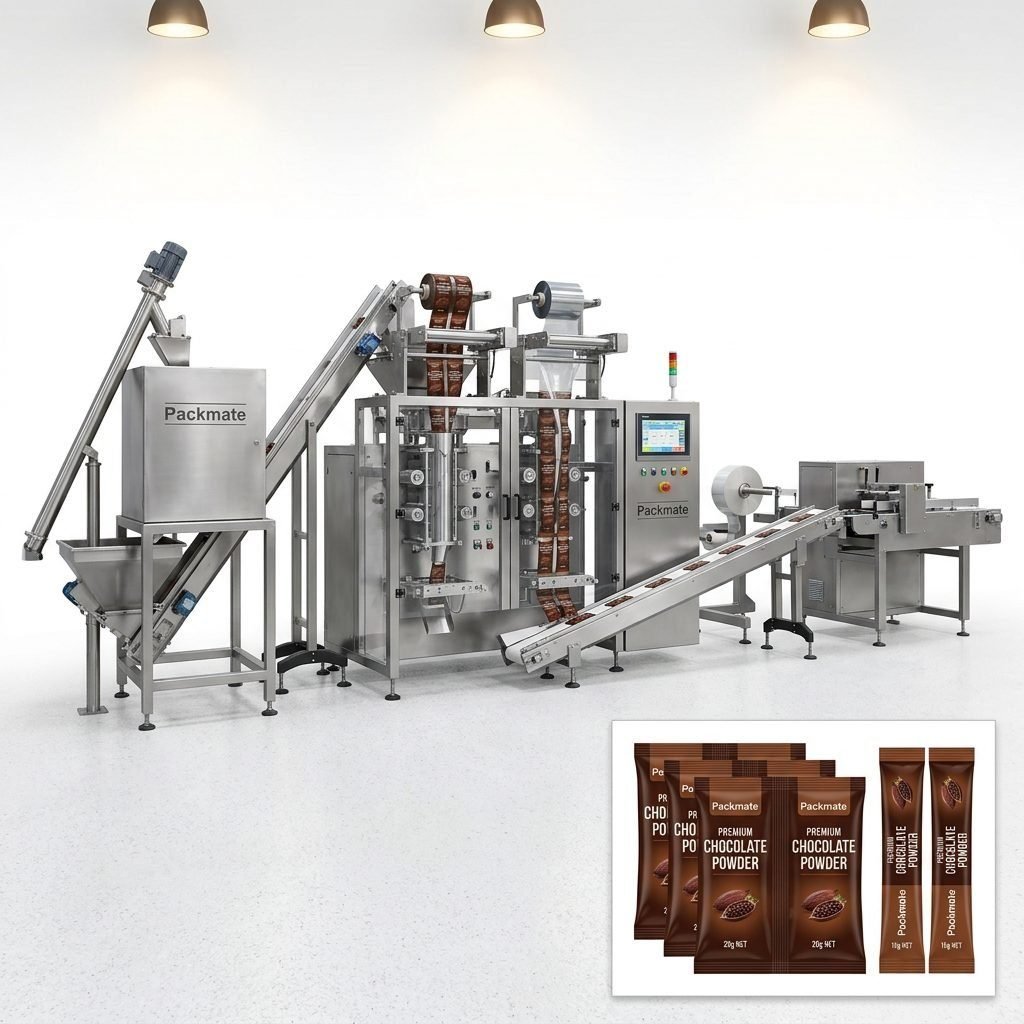
- Extensive Product Range: Offering more than 50 machine models, including specialized sachet and stick pack machines and versatile bag and pouch packaging machines.
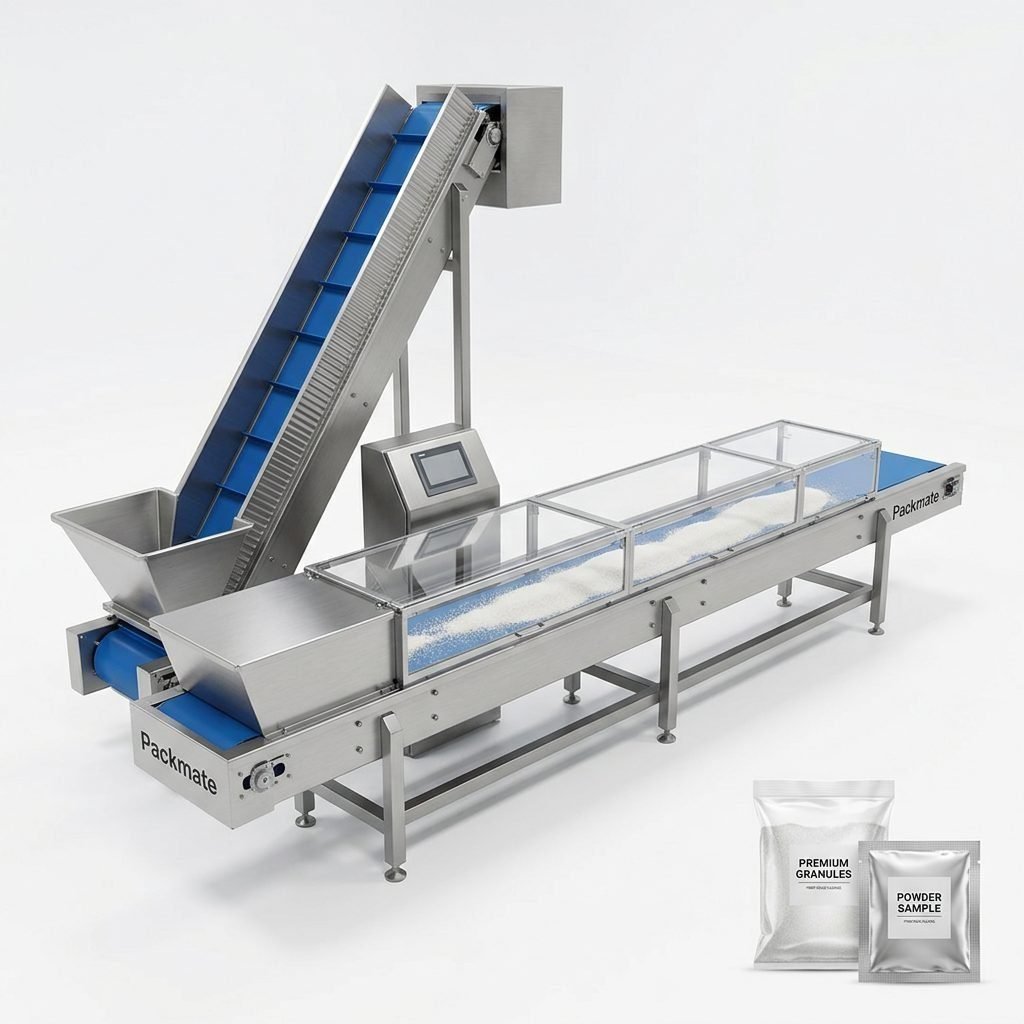
- Turnkey Solutions: Providing complete lines from weighing and feeding to final packaging, ensuring compatibility and peak performance.
- Global Support Network: Serving clients worldwide with localized service and parts support, minimizing response times.
- Continuous R&D: A dedicated team of 125+ professionals drives technological advancement, adapting to new market demands like sustainable materials.
Innovation Driven by Customer Needs
The development of multi-lane stick pack machines in 2012, a direct response to growing market demand for higher output, is a testament to Packmate’s customer-centric innovation. This focus ensures their equipment, such as advanced weighing and packaging systems, solves real-world production challenges, enhancing both speed and accuracy for products like granules, powders, and liquids.
Selecting Your Ideal Equipment Partner
Choosing a supplier is a strategic decision. Look beyond the initial price quote. Evaluate the supplier’s industry experience, review their project case studies, and assess their testing and quality control protocols. A visit to their manufacturing facility or a demonstration with your own materials can provide invaluable insights.
Consider the total cost of ownership, which includes energy efficiency, maintenance costs, and the potential for future upgrades. A partner that offers scalable solutions allows your business to grow without requiring a complete system overhaul.
Pro Tip: Always request references from existing clients in a similar industry. Their firsthand experience with machine performance, reliability, and supplier responsiveness is the most credible evaluation metric.
The Importance of Service and Training
Even the most reliable equipment requires maintenance. Top suppliers provide extensive installation supervision, comprehensive operator and maintenance training, and clear documentation. This empowers your team to handle routine procedures and minor troubleshooting, ensuring sustained efficiency. A robust service plan is not an add-on but a fundamental component of a reliable solution.
Future Trends in Shrink Packaging
The industry is moving towards greater sustainability and connectivity. Expect increased demand for equipment that handles mono-material and recyclable films efficiently. The integration of Industry 4.0 principles, such as IoT sensors for predictive maintenance and data analytics for process optimization, will become standard. Suppliers at the forefront, like Packmate, are already incorporating these smart technologies into their designs to future-proof their clients’ investments.
Automation will continue to reduce labor dependency, with more sophisticated vision systems for quality inspection and robotic integration for handling. Flexibility will also be key, as markets demand shorter production runs and more frequent product changes.
Frequently Asked Questions (FAQs)
What types of products are best suited for shrink packaging?
Shrink packaging is incredibly versatile. It is ideal for bundling multi-packs (bottles, cans), securing promotional items together, providing tamper-evident seals, and creating sleek, contoured packages for food items, pharmaceuticals, cosmetics, and hardware. It works well with rigid, semi-rigid, and irregularly shaped items.
How do I determine the right machine speed for my production line?
Machine speed (packages per minute) should be matched to your upstream and downstream line speed. Consider your peak production demands, desired buffer capacity, and future growth. A reliable supplier will help you model this based on your product specifics, film type, and seal requirements to avoid over- or under-investing.
What is the difference between a sleeve wrapper and a shrink bundler?
A sleeve wrapper typically applies a loose sleeve of film around a product or group of products, which then passes through a heat tunnel to shrink the film tightly. A shrink bundler often forms the film into a bag or pouch around the products before sealing and shrinking. Bundlers are common for multi-packs, while sleeve wrappers are used for single items or trays.
How important is energy efficiency in a shrink tunnel?
Extremely important. Shrink tunnels can be significant energy consumers. Modern efficient tunnels use insulated cabinets, precise zonal temperature control, and efficient heating elements (like ceramic infrared) to minimize heat loss and reduce energy consumption by 20-40% compared to older models, offering a rapid return on investment.
Can existing packaging lines be upgraded with new shrink equipment?
Yes, in most cases. A top supplier will audit your current line layout, conveyor speeds, and control systems to design an integrated upgrade. This can involve retrofitting a new, more efficient shrink tunnel, adding automatic film dispensers, or integrating smart controls without needing to replace the entire line.