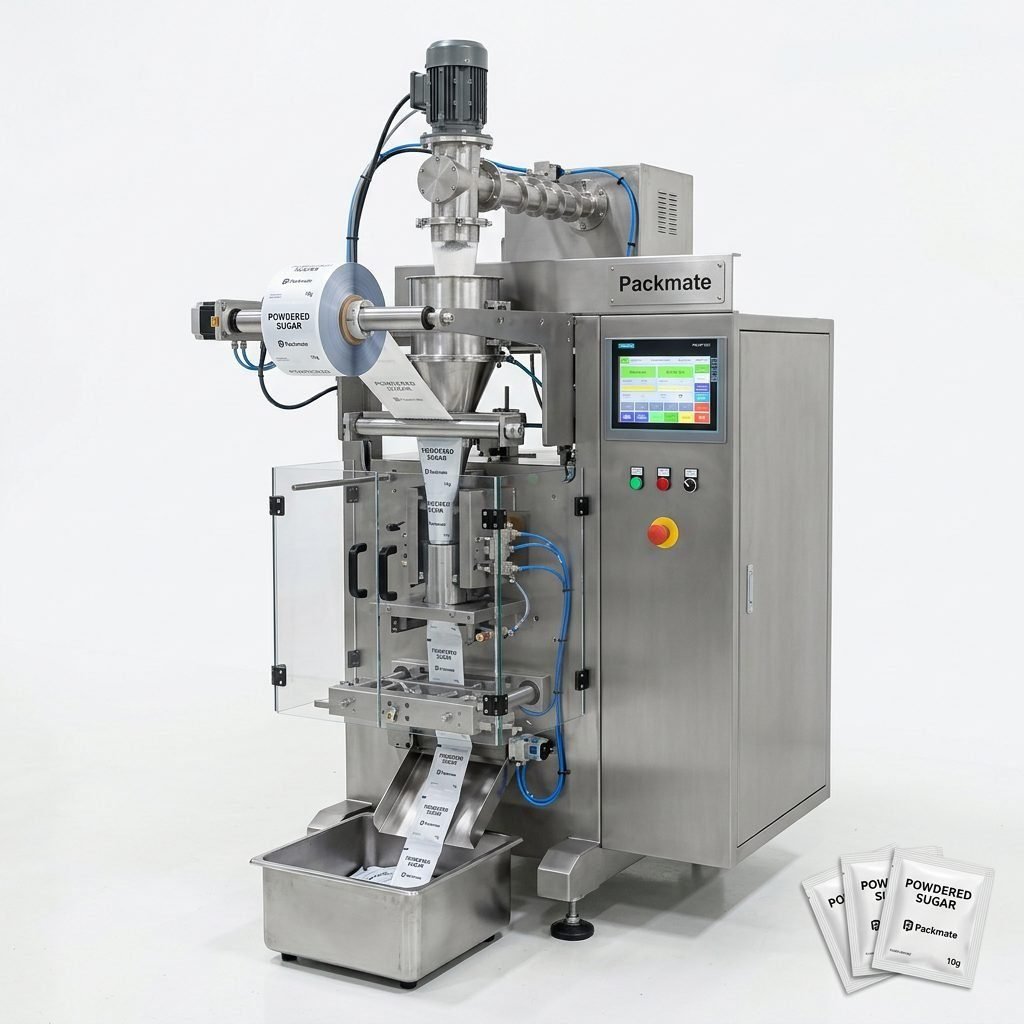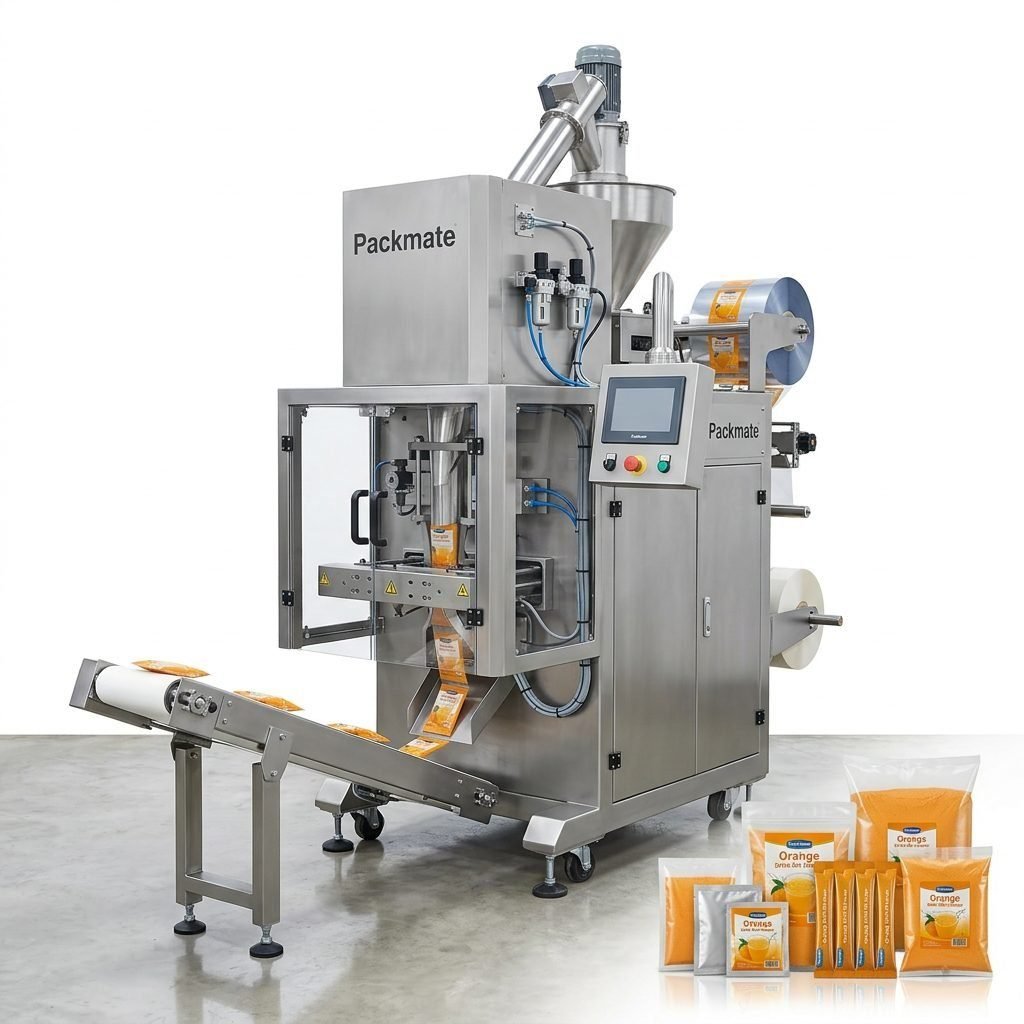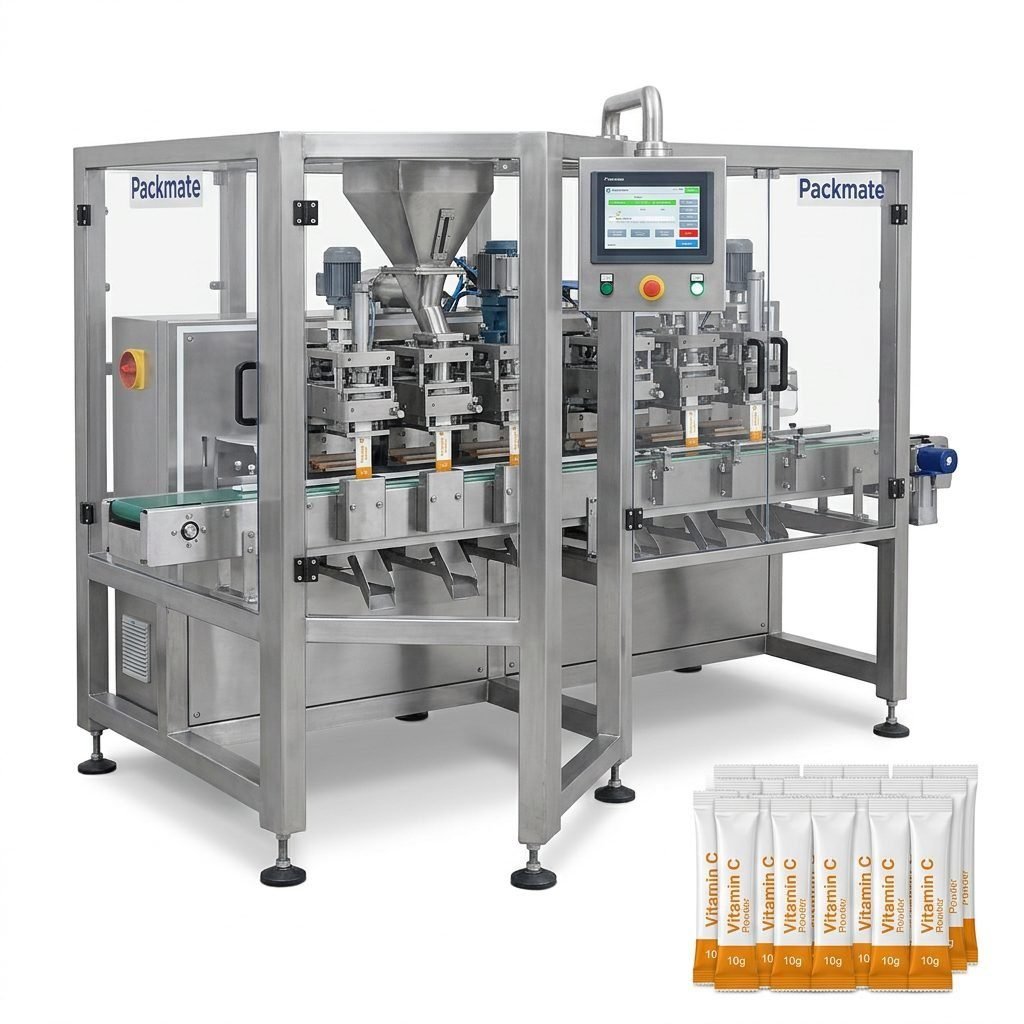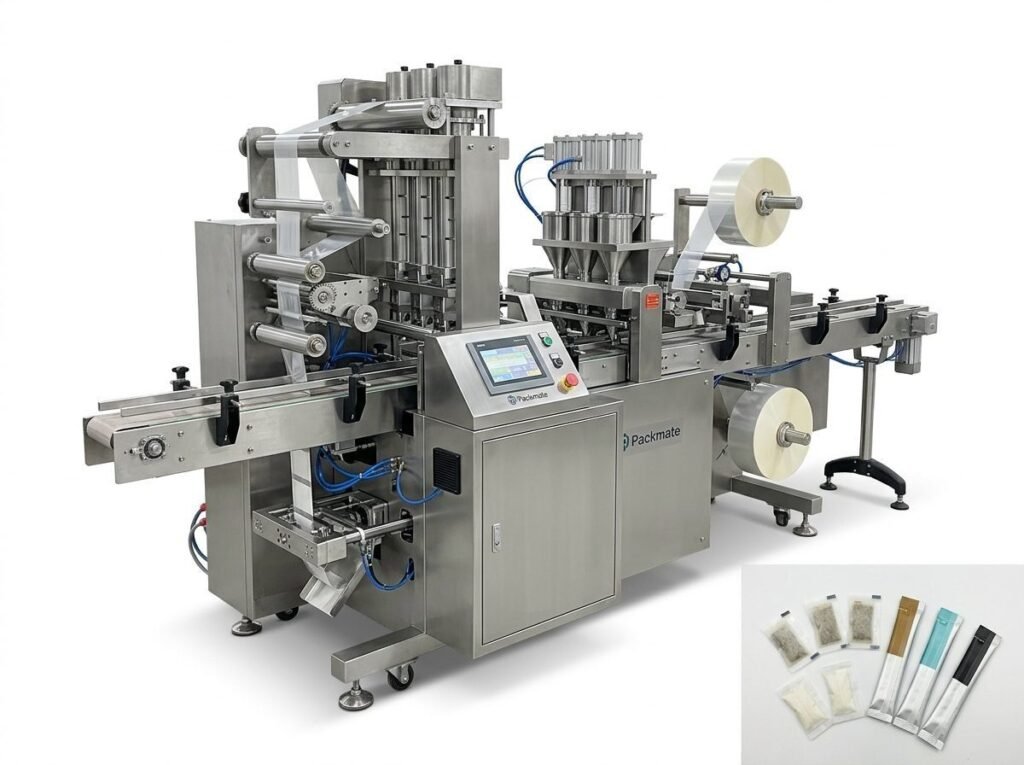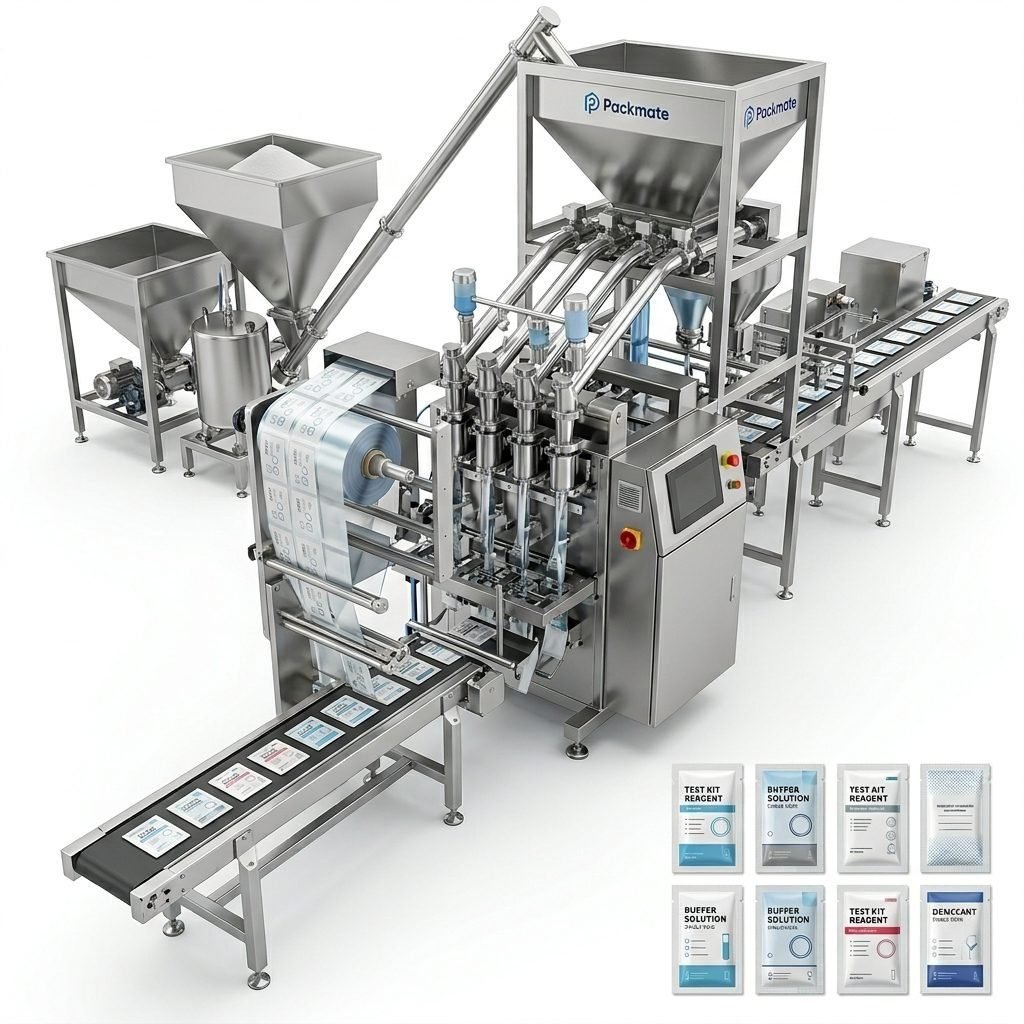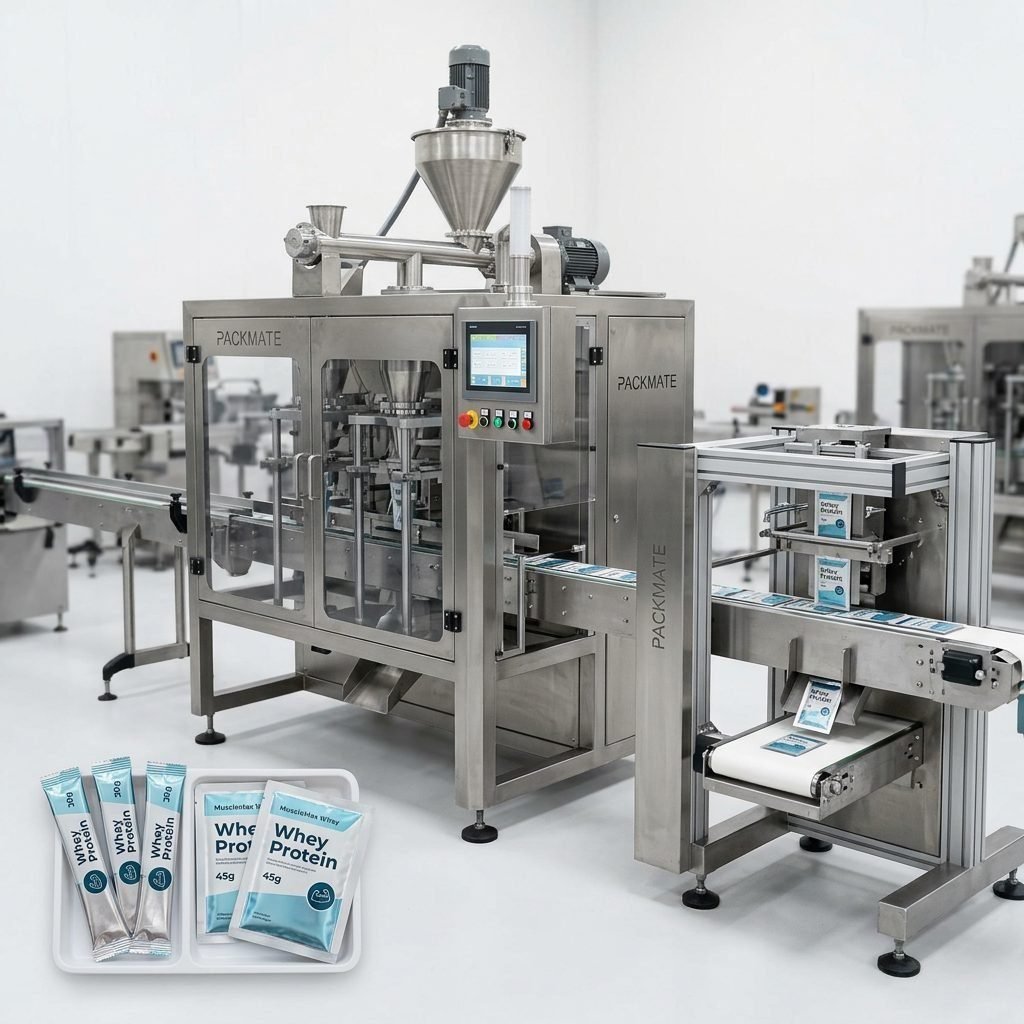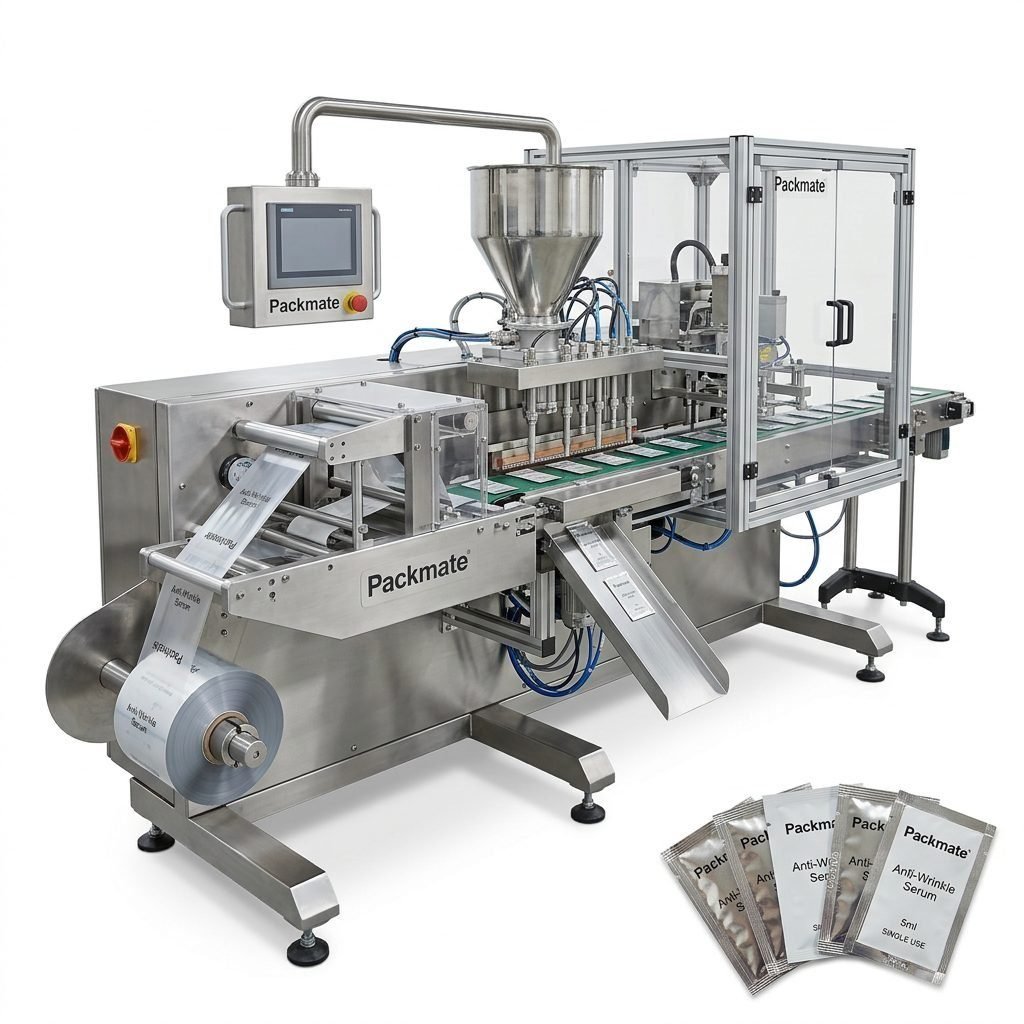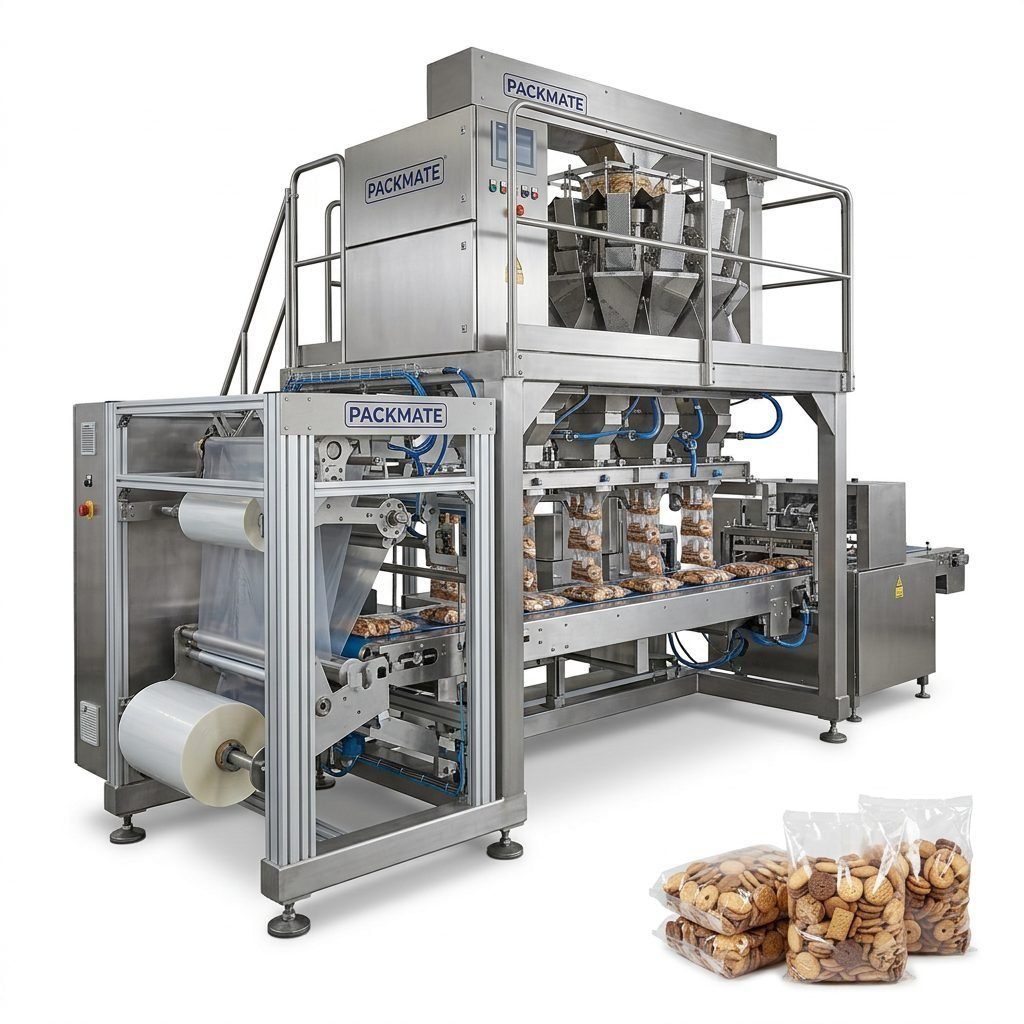
In the dynamic world of food manufacturing, the reliability and efficiency of your packaging line are non-negotiable. Choosing the right food packaging equipment supplier is a critical business decision that impacts productivity, product integrity, and ultimately, your bottom line. This guide explores the hallmarks of top-tier suppliers and the reliable industrial solutions they provide, ensuring your operations are built on a foundation of quality and innovation.
What Defines a Top Food Packaging Equipment Supplier?
The market is filled with vendors, but true leaders distinguish themselves through a combination of factors that guarantee long-term value and operational peace of mind.
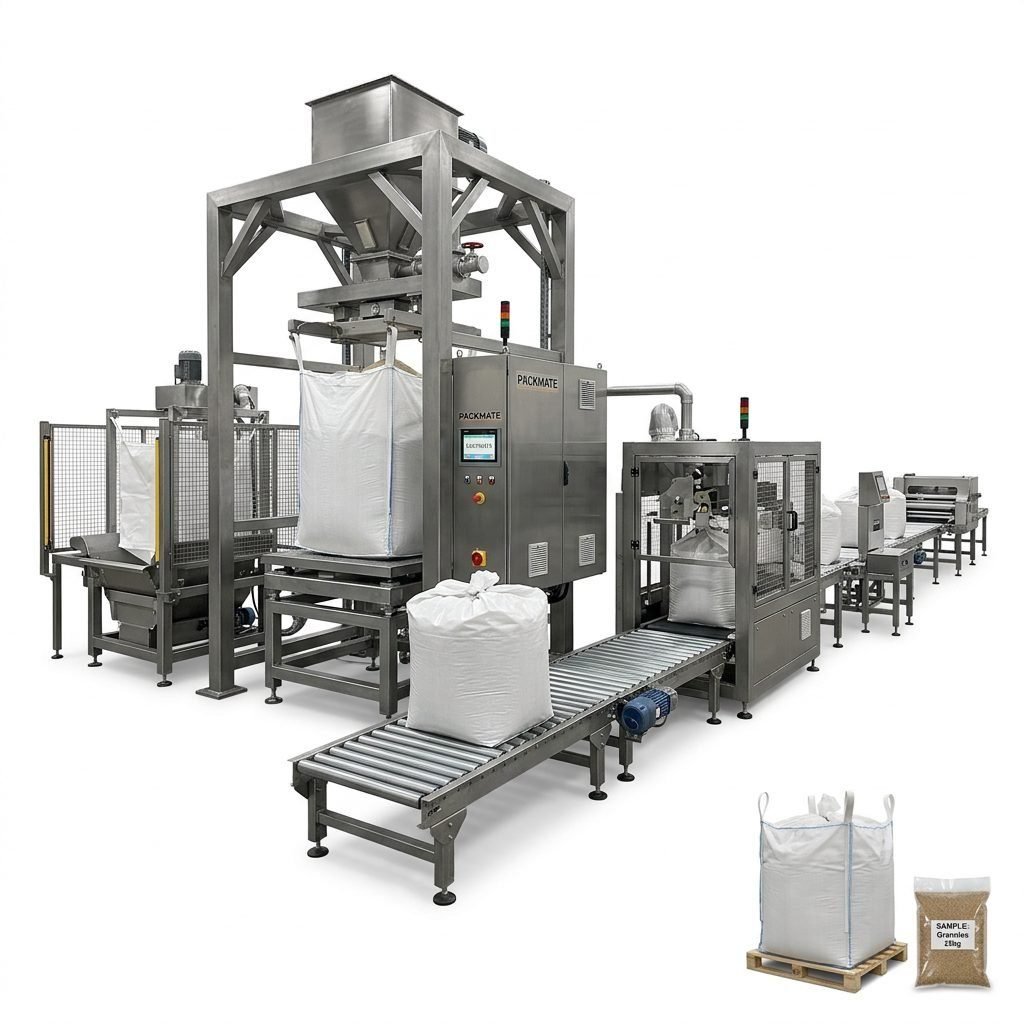
A premier supplier goes beyond simply selling machines. They act as a strategic partner, offering comprehensive turnkey packaging solutions. This means they provide everything from initial consultation and machine design to installation, training, and ongoing technical support. Their goal is to deliver a seamless, integrated system that solves your specific packaging challenges, whether you’re handling granules, powders, or liquids.
Core Pillars of Excellence
When evaluating potential partners, focus on these essential pillars:
Proven Expertise & Industry Experience: Decades of operation translate into deep practical knowledge. A supplier with over 30 years in the field, like Packmate Machinery, has navigated countless industry shifts and technical challenges, refining their equipment and processes to deliver unmatched reliability.
Commitment to Innovation: The packaging industry evolves rapidly. Leading suppliers invest in research and development to incorporate the latest automation, precision weighing, and hygienic design technologies into their packing machines.
Robust Manufacturing Capabilities: In-house control over production is key. A modern facility spanning 20,000㎡, equipped with over 100 advanced production and testing units, ensures rigorous quality control at every stage, from component machining to final assembly.
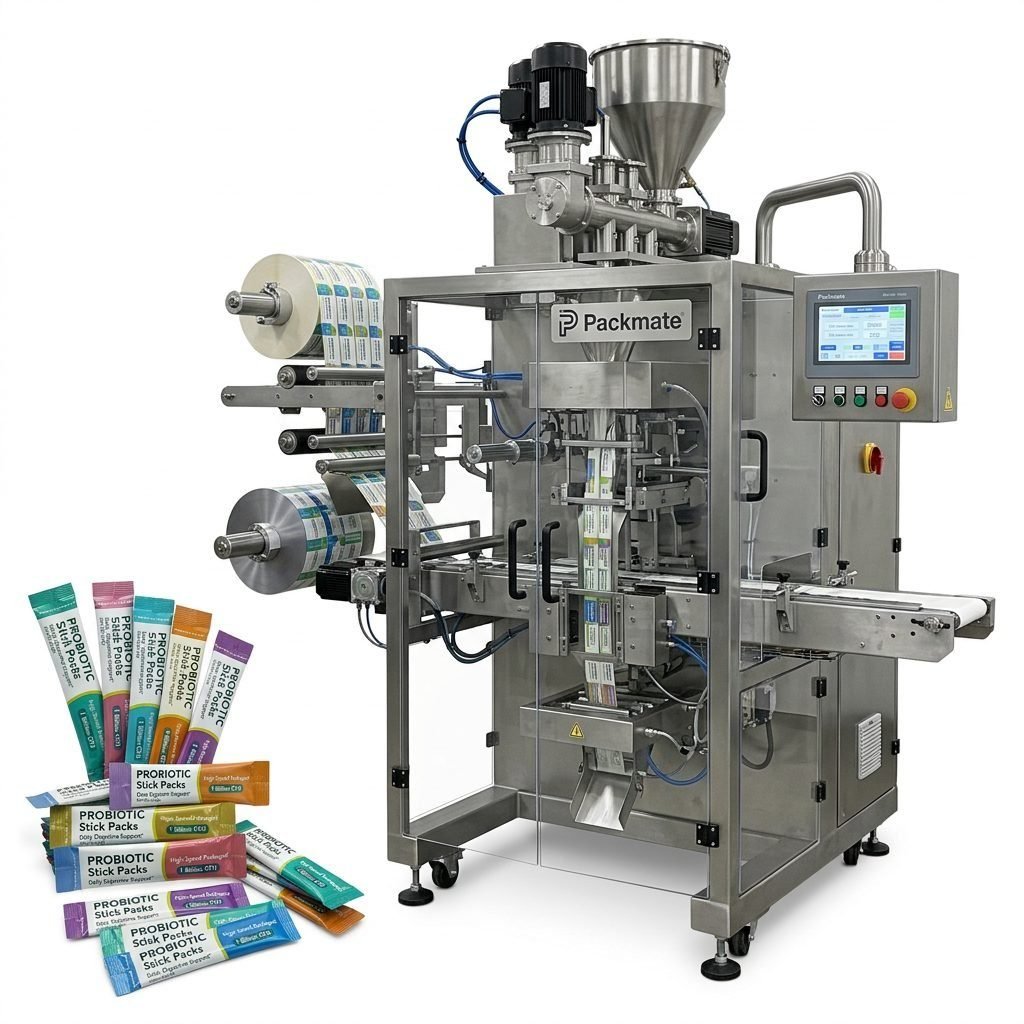
Extensive & Versatile Product Range: A diverse portfolio, often exceeding 50 machine models, indicates the ability to cater to various needs. This includes specialized lines for sachet and stick pack machines, as well as systems for larger bag formats.
Reliable Industrial Solutions for Modern Demands
Today’s food producers require equipment that is not only fast but also smart, adaptable, and hygienic. Reliable solutions address these core demands head-on.
Precision and Consistency
For products sold by weight or volume, accuracy is paramount. Advanced weighing and packaging systems utilize multi-head weighers and volumetric fillers to minimize giveaway and ensure every package meets strict regulatory and customer specifications. This precision protects your profit margins and brand reputation.
Hygiene and Safety by Design
Food safety is the highest priority. Top-tier equipment features easy-clean designs, stainless-steel contact surfaces, and enclosed mechanisms to prevent contamination. This design philosophy is crucial for meeting global food safety standards (like HACCP, GMP) and is a fundamental aspect of reliable industrial solutions.
Key Takeaway: The most reliable machinery integrates seamlessly into your existing workflow. Look for suppliers who offer customizable solutions and full production line integration, ensuring that your new filling and packaging line works in perfect harmony with upstream and downstream processes.
The Importance of After-Sales Support
True reliability is tested after the sale. A supplier’s commitment is measured by their support network. This includes:
• Comprehensive Training: Empowering your team to operate and perform basic maintenance on the equipment.
• Readily Available Spare Parts: Maintaining an extensive inventory to minimize downtime.
• Responsive Technical Service: Offering remote diagnostics and rapid on-site support from a professional team.
This holistic approach to service transforms a equipment purchase into a long-term partnership for growth.
Building on a Foundation of Trust and Heritage
The story behind a supplier often reflects their values and dedication. Many industry leaders, such as Packmate Machinery, began with a founder’s vision to solve practical problems through automation. From a small workshop in 1993, driven by a passion for enhancing productivity, the company formally incorporated in 2003. This journey from a dedicated idea to a global supplier underscores a culture of perseverance, innovation, and hands-on engineering excellence that continues to drive their mission today.
Global Reach, Local Understanding
While the core principles of quality and reliability are universal, the best suppliers understand and adapt to regional market nuances. Serving an international clientele requires not just shipping machines worldwide, but also understanding diverse packaging regulations, consumer preferences, and logistical challenges. This global perspective, combined with a commitment to collaborative problem-solving, is what makes a supplier a true global partner.
Selecting a food packaging equipment supplier is a strategic investment. By prioritizing partners with deep expertise, a commitment to innovation, robust manufacturing, and unwavering after-sales support, you secure more than just machinery—you gain a reliable industrial solution that drives efficiency, ensures quality, and supports your business’s growth for years to come. The right partnership empowers you to meet market demands with confidence and agility.
Frequently Asked Questions (FAQs)
What types of products can your packaging machines handle?
Our equipment is engineered to reliably package a wide range of dry and liquid food products, including granules (like coffee, sugar), powders (spices, milk powder), and viscous liquids (sauces, oils). We offer specific solutions for sachets, stick packs, and larger pouches.
How do you ensure the hygiene and food safety of your equipment?
Hygiene is a core design principle. We utilize food-grade stainless steel for product contact parts, incorporate easy-clean, open-frame designs, and design systems to meet international food safety and hygiene standards, supporting our clients’ HACCP and GMP compliance.
Do you offer complete production line solutions or just individual machines?
We specialize in providing complete, integrated turnkey packaging solutions. This includes everything from the primary packaging machine (like a form-fill-seal unit) to upstream feeders, downstream cartoning, and all necessary conveying and control systems for a seamless operation.
What kind of after-sales support and training do you provide?
Our support includes comprehensive on-site installation and operator training, a readily available inventory of spare parts, and access to responsive technical service for both remote troubleshooting and on-site maintenance, ensuring minimal downtime.
Can your machines be customized for our specific packaging needs?
Yes, we understand that one size does not fit all. We work closely with clients to understand their unique requirements and offer significant customization options for bag sizes, shapes, filling methods, and integration with existing factory equipment to create an optimal solution.